UV Digital Printer Factory: A Behind-the-Scenes Look at Production and Quality Control
2026-11-21
Most people assume a UV digital printer is just another machine bolted together on a busy assembly line. Step inside the floor where Danmajet builds its printers, and that assumption falls apart quickly. From the way frames are milled to the final inkjet nozzle alignment, every stage carries a level of scrutiny you rarely see in mass production. This behind-the-scenes look reveals why quality control here feels less like a checklist and more like a quiet obsession.
Raw Frame Inspection Before the First Bolt Goes In
Before anything gets threaded or torqued, the bare frame is checked against the build jig with straightedges, plumb lines, and a few well-placed measuring points. It is more than a quick glance for obvious bends. Tube alignment, dropout spacing, and head tube angle are verified while the frame is still untouched, because even a small pull from welding can move a mount just enough to cause trouble later. Any sign of shipping damage or a fixture shift gets written down before it has a chance to hide under paint or powder.
Weld starts and stops get looked at under bright light, not just for appearance but for undercut, porosity, or incomplete fusion where a crack could begin. Threaded bosses and bottle mounts are chased by hand to catch overspray or rough edges that would chew through a bolt. This is the point where a suspect joint costs an hour of rework instead of a full strip-down after the first ride. If the raw frame does not pass here, no amount of careful assembly will make it right.
Where Printhead Alignment Becomes a Factory Discipline
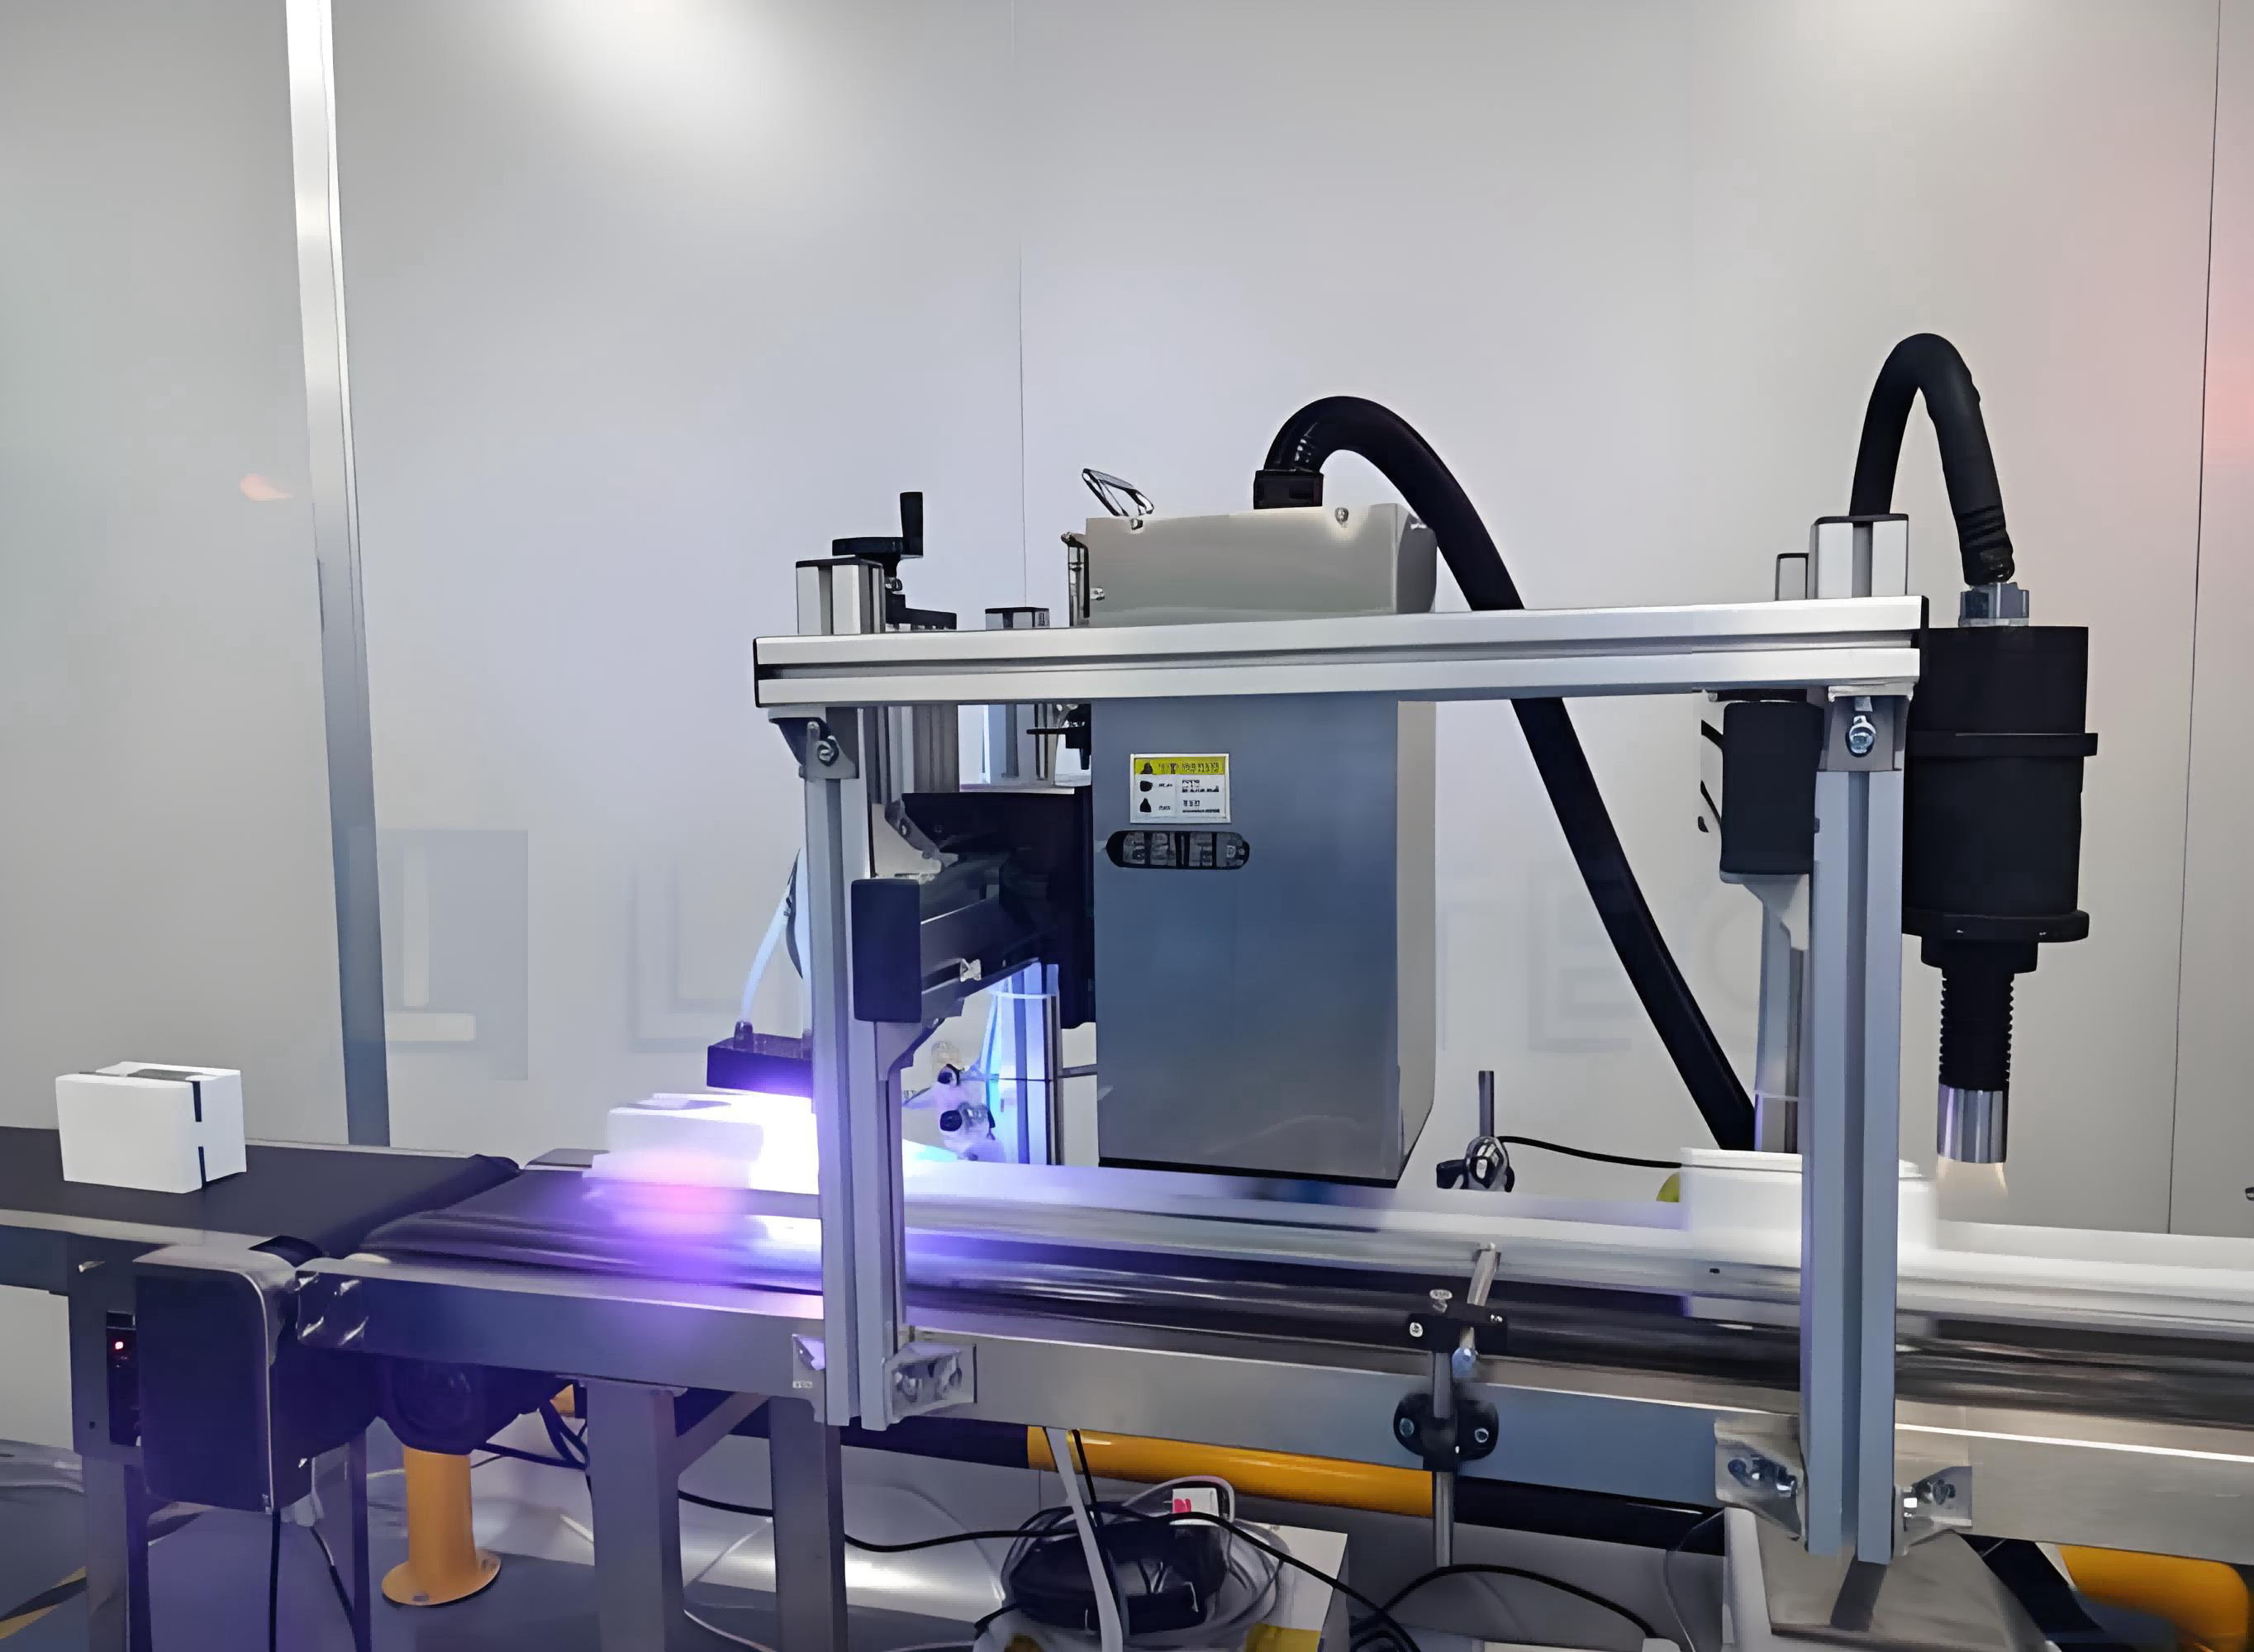
On high-volume print lines, alignment is rarely treated as a repair task anymore. It gets folded into the same daily rhythm as torque checks and sensor cleaning, with line leads signing off on measured offsets before a shift starts. The idea is not to chase perfection after a defect appears, but to keep the printhead from drifting far enough to matter in the first place.
The discipline shows up in small, repeated habits. Checking ambient temperature before touching the carriage, recording a baseline after a substrate change, and comparing today's readout against a rolling three-day average instead of a fixed ideal are all part of the shift. These routines turn a finicky calibration into something closer to statistical process control, where a few microns of drift becomes a warning sign rather than an emergency.
What often separates a stable line from one that fights recurring banding is not better hardware, but the refusal to let alignment depend on an operator's feel. Technicians follow the same written sequence, use the same target, and log the same fields every time. Over enough shifts, that consistency builds a history that makes failures predictable—and alignment, strangely enough, becomes one of the quieter disciplines on the floor.
Ink System Calibration Without Shortcuts or Guesswork
Calibration starts with the printer's native behavior, not with a preset someone else built for a different machine, ink batch, or humidity level. A printed target is measured, and the resulting numbers are fed back into the system before any profile is generated. Skipping this step or copying values from a forum tends to produce flat shadows, blocked highlights, or color that drifts within a few days.
The useful routine is slower but repeatable: set the ink limits where the media stops accepting more pigment, linearize the channels so each step moves predictably, and check the gray axis under the actual viewing light. Small adjustments matter more than large corrections, because an overcorrected curve often looks right on one test image and wrong on everything else.
Calibration records also deserve attention. Logging temperature, humidity, head height, ink lot, and media batch turns a one-time fix into a diagnostic tool when output shifts later. That kind of discipline feels tedious, but it removes the guesswork that usually gets blamed on profiles, RIP settings, or the inks themselves.
The Burn-In Room That Separates Reliable Printers from the Rest
Freshly assembled printers are moved into a room where the daily routine is deliberately harder than any office workload. Long print runs mix dense text, full-bleed graphics, labels, and blank pages while temperature and humidity shift enough to stress solder joints, plastic frames, and paper rollers. Some units are power-cycled mid-job or fed slightly worn media to see how the paper path reacts. A small misfeed, faint banding, or unstable color alignment is enough to pull a unit from the line.
The value shows up after weeks of real use. Printers that survive this phase tend to hold registration, avoid phantom jams, and keep their fusers from drifting under heat. It is not a quick final test; it is a window into early electronic and mechanical failures that would otherwise appear in a customer's office. Shortening or skipping this step saves time at the factory, but it shifts the cost to repair tickets and returned units instead.
Final Quality Gates That Check More Than Print Resolution
Resolution tells you how many dots fit in an inch, but it says almost nothing about how those dots hold up once ink meets substrate. A final gate here means pulling samples from the middle of the run, not just the start, and checking for banding in large flat areas, bronzing on heavy ink loads, or a color shift that only shows up after the sheet has cooled. The same file can look completely different on two stocks with identical stated print resolution, so side-by-side comparison under the actual shop lighting matters more than a magnifier on a test patch.
The next gate moves past the printed surface to finishing and assembly. A job can have flawless output at 1200 dpi and still fail because trim marks drifted, creep pushed inner pages too close to the fold, or the cover laminate added just enough stiffness to crack along the spine. These are physical checks: fanning the book to see the gutter, stacking folded signatures to compare edges, measuring bleed after cutting instead of trusting the preset. Resolution will never catch a misaligned score or a cover that wraps short by a millimeter.
Durability and hand feel are the quiet part of the gate that gets skipped when people fixate on sharpness. Rub a printed area with a clean finger to test adhesion, check fold lines against a backlight for cracked ink, and set two copies under different lighting to catch metameric mismatch. Some coats look perfect head-on but reveal streaks at a low angle. The final gate should include these small, unglamorous checks because a print that looks razor-sharp on screen and under loupe can still feel cheap, scuff too easily, or change color by the window.
Crating and Shipping Without Undoing the Calibration
Moving a calibrated instrument from one bench to another often feels like a gamble—every bump, tilt, or vibration threatens to undo hours of careful adjustment. The most reliable approach starts with locking down any movable stages, gimbals, or focusing mechanisms before the crate is even opened. Soft foam inserts cut to the exact footprint of the device do more than cushion; they prevent micro-shifts that accumulate during transit and quietly push a system out of tolerance.
A common mistake is treating the shipping container as a generic box rather than an extension of the calibration environment. Humidity-absorbing packs, anti-static liners, and rigid corner braces all work together to keep the instrument in the same physical state it was in when the last adjustment was made. If the device has a transit mode or locking screw, engage it before powering down—many precision tools rely on mechanical stops to preserve optical or electrical alignment.
Finally, consider the route itself. Hand-carrying a lightweight sensor in a padded case may preserve calibration better than sending it through a freight network with repeated drops and temperature swings. When shipping is unavoidable, mark the crate with orientation indicators and use shock-logging labels to verify that the journey stayed within acceptable limits. The goal is not just to protect the hardware, but to make the return to service as close to the original calibrated state as possible.
FAQ
The floor is divided into stations rather than a single moving line. One team mounts the steel gantry and checks rail alignment with a dial indicator, another installs the ink system and negative pressure lines, and a third handles wiring looms before the machine rolls to the calibration bay.
Each printhead gets a nozzle check on a dedicated bench that records missing or deflected jets. If a head passes, it is flushed with a storage fluid and installed immediately. The serial number and nozzle check report stay with the machine file for traceability.
Printheads, UV LED arrays, and linear guides get the most attention. The team checks printhead nozzle plates under magnification, measures UV intensity across the lamp face, and verifies rail straightness before any of these parts are allowed into inventory.
It goes through a staged runoff. The machine prints a full-width color chart for head alignment, runs a continuous job for several hours to catch ink starvation or overheating, and then prints adhesion and scratch tests on the actual substrates the customer plans to use.
A radiometer is placed at multiple points across the lamp to map intensity and uniformity. The team also runs a cure test with a hard-cure ink on difficult substrates. If the surface remains tacky or adhesion fails, the lamp height, power, or carriage speed is adjusted and the test is repeated.
The biggest differences are frame rigidity, cable routing, and how much time is spent on alignment. A better machine uses a heavier welded frame that is stress-relieved before machining, keeps ink and power lines separated, and goes through longer thermal stabilization tests so the print position does not drift.
Yes, many orders are built to spec. The factory can widen the bed, add extra printhead channels for white or varnish, or configure the machine for rotary printing. The sales engineer confirms the changes with the production team before the frame enters the welding stage.
Conclusion
A UV flatbed printer starts taking shape long before any electronics are mounted. Incoming steel frames are checked for twist, weld consistency, and machined flatness, because a half-millimeter deviation at the base turns into visible banding once the carriage is moving. Printhead alignment is treated less like a setup task and more like a standing rule on the floor: each head is seated against reference pins, measured with dial indicators, and rechecked after the gantry is tensioned. The ink path receives the same scrutiny. Negative pressure, temperature compensation, and waveform settings are adjusted per batch of ink rather than left at default values, so viscosity shifts do not quietly damage the heads.
After assembly, every machine enters a burn-in room where it runs unattended jobs overnight and through thermal cycles that mimic a warm print shop. Failures here are logged, traced to a station, and corrected before the printer is allowed to move on. Final inspection goes beyond nozzle checks and resolution targets: technicians look for cable rub, loose grounding, uneven vacuum zones, and any rattle that could become a service call later. When the printer passes, the factory does not simply wrap it in foam. Carriage locks, beam supports, and custom crating hold the aligned components in place so a rough truck ride does not undo weeks of calibration. The result is not just a machine that prints well on day one, but one that stays predictable after installation.
Contact Us
Contact Person: Jacky
Email: [email protected]
Tel/WhatsApp: 086 15000607053
Website: https://www.danmajet.com