Ultrasonic Spray Pyrolysis System Brands to Trust for Thin-Film Coating
2026-10-28
Thin-film coating is equal parts art and precision—choose the wrong ultrasonic spray pyrolysis system, and you'll spend more time troubleshooting than innovating. While a handful of brands dominate lab benches and pilot lines, few combine repeatable droplet control with genuinely responsive process support. That's where the noise thins and names like Siansonic start earning their place. If you've been weighing throughput against uniformity, or wondering which manufacturers actually stand behind their atomization claims, this guide cuts through the marketing fog to spotlight the brands worth your trust.
Brands That Actually Deliver Uniform Thin Films
When you compare test results rather than marketing copy, a few names keep showing up with genuinely even coating thickness. 3M's automotive and architectural films tend to hold within a tight tolerance, and their optical clarity doesn't suffer from the wavy edges you see in cheaper alternatives. XPEL and LLumar also earn their reputation here—their self-healing and ceramic lines apply without the patchy, orange-peel texture that plagues budget rolls. What sets these apart isn't just the raw material, but the consistency of the adhesive layer and the controlled tension during manufacturing.
On the DIY side, Gyeon and CarPro offer ceramic coating kits that, when wiped correctly, level out into a surprisingly uniform film. The difference shows under a swirl-finder light: no high spots, no thin streaks where the coating pulled away. For paint protection films, SunTek's reaction layer doesn't just look smooth on day one; it maintains that evenness after months of heat cycling. You'll notice the same pattern in window tint—brands like FormulaOne and Huper Optik don't leave the subtle vertical bands that make night driving a headache.
One practical way to spot a brand that actually delivers is to look at how they handle edge wrapping and complex curves. Cheap films stretch unevenly, thinning out over peaks. The trusted names invest in polymer blends that retain viscosity during installation, so the film doesn't sag or puddle. Whether it's a full front clip on a sports car or a curved glass balustrade, the finished layer looks like it was sprayed on, not draped. That's the real test of uniform thin film technology.
What to Look for in a Spray Pyrolysis Nozzle Before You Commit
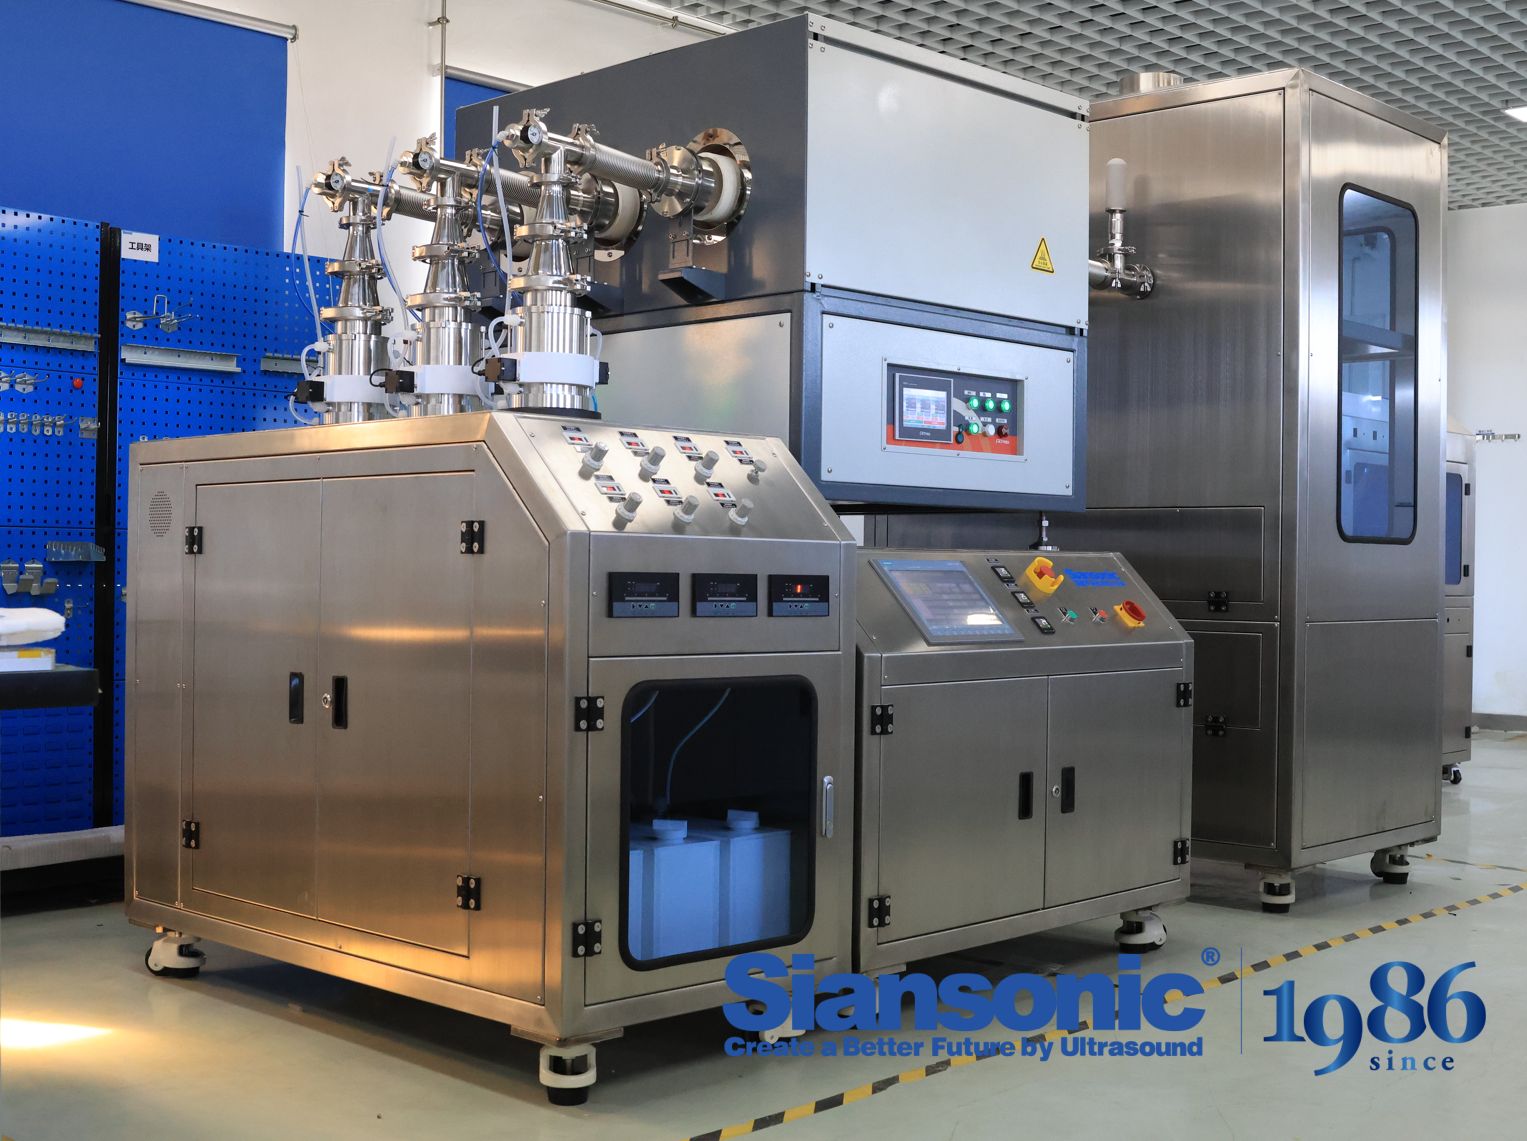
A nozzle that can't hold a steady cone angle or produces uneven droplet sizes will ruin film thickness before you ever get to annealing. Look for designs with adjustable air/liquid mixing and verified droplet size ranges under your actual feed rate—spec sheets from water tests rarely translate to viscous or precipitate-prone precursors. Pay attention to the liquid orifice diameter and how it pairs with your intended solvent system; too narrow and you'll battle constant pressure spikes, too wide and you sacrifice atomization quality.
Clogging is the silent killer of spray pyrolysis runs. If the nozzle requires complete disassembly to clear a blockage, or has internal dead zones where solute can crystallize, you'll spend more time cleaning than coating. Prefer nozzles with a straight-through liquid path, minimal internal gaskets, and the option to pulse solvent between runs. Also check thermal stability of the tip and O-rings—some plastics soften above 200°C and lead to drift in spray geometry, while a stainless or ceramic tip can handle repeated heating cycles without deforming.
The Quiet Engineering Details Behind Reliable Ultrasonic Systems
Most ultrasonic systems look nearly identical on the outside — a generator, a transducer, a horn, some cables. But the real differences hide in the mundane details. Cable impedance matching, for instance, rarely gets mentioned in marketing sheets. Yet a slight mismatch between the generator output and the transducer’s resonance point doesn’t just waste energy; it silently degrades amplitude stability over hours of continuous duty. Engineers who have spent time on factory floors know that inconsistent weld quality often traces back to a connector that was “good enough” on paper but thermally drifts after thirty minutes.
Another quiet killer is mechanical grounding. A horn that isn’t perfectly seated against the booster can vibrate at a secondary node, creating micro-fractures that don’t show up in initial testing. The fix isn’t glamorous — lapping the contact surfaces to within a few microns and re-torquing in a specific sequence. But that’s what separates systems that run for five years without a rebuild from ones that need new studs every quarter.
Power supply design matters more than most realize too. Cheap ultrasonic generators deliver raw AC into a rectifier and call it a day, but that lets line noise modulate the ultrasonic frequency. The result? Amplitude ripple that looks fine on an oscilloscope average but wreaks havoc on thin films or delicate wire bonding. A reliable system filters and regulates the DC rail well beyond the datasheet minimums, then monitors the transducer’s impedance in real time to compensate for temperature-induced shifts. These are the details that never make the brochure, but they’re the first thing you notice when a line runs for six months without a single fault light.
Where Thin-Film Coating Demands Push Brands to Their Limits
Thin-film coating rarely gets the spotlight, but it quietly decides whether a phone screen survives a drop or a camera lens delivers crisp images in harsh light. The demands are brutal: layers measured in nanometers must adhere perfectly to curved glass, resist abrasion from keys and coins, and maintain optical clarity across thousands of thermal cycles. Brands that treat this as a commodity soon find their products failing in the field, while those who push the limits discover that tiny material choices cascade into user-visible differences in durability and glare control.
The real pressure comes from balancing competing requirements. A coating that improves scratch resistance might introduce haze or color shift, and one that reduces fingerprints can wear unevenly under repeated swipes. Engineers test dozens of formulations on curved edge displays, where deposition angles change and stress concentrates. The brands that succeed are often the ones willing to invest in custom sputtering targets and iterative process control, rather than accepting off-the-shelf solutions that fail on the corners of a folded device or the barrel of a compact zoom lens.
Reliability testing reveals another layer: a coating can pass initial specs but degrade after six months of pocket abrasion or salt spray. Forward-leaning brands now simulate five years of wear in weeks, using robotic fingers with varied pressure and humidity cycling. Those who push boundaries treat thin-film coating as a performance feature, not a checklist item, and their products show it in the tiny scratches that never appear and the crisp images that hold up long after launch.
How Real Users Separate Trustworthy Suppliers from the Rest
When someone has been burned by a supplier who promised fast shipping and then disappeared for three weeks, they stop believing polished websites. Instead, they pay attention to tiny inconsistencies that most marketing teams miss. A real user might notice that a supplier's invoice format changes slightly between orders, or that their customer service replies become shorter right after a payment clears. These small shifts are often more telling than any certificate or badge on a homepage.
For many buyers, the decision comes down to how a supplier behaves when something goes wrong. A trustworthy partner doesn't pretend that delays never happen—they proactively send a message with a revised timeline and a clear explanation. Users also tend to compare what a supplier says about lead times with what independent forums and review threads actually report. If there's a gap between the polished sales pitch and the messy reality described by past customers, that gap becomes the deciding factor.
Over time, experienced buyers develop a kind of pattern recognition. They look for suppliers who ask clarifying questions before accepting an order, because that shows attention to detail. They also appreciate suppliers who are willing to send a short video of the actual product or warehouse instead of relying on stock photos. Trust isn't built by a perfect first impression—it's built by a series of small, verifiable actions that match what a supplier claims on paper.
A Practical Checklist for Comparing Ultrasonic Spray Pyrolysis Builds
When you line up two ultrasonic spray pyrolysis rigs side by side, the spec sheet rarely tells you which one will actually hold a stable plume over a six-hour deposition. Start with the nozzle itself: check the resonant frequency, but more importantly watch how the mist behaves at the edge of the spray cone. Some builds produce a tight, almost dry halo around the central wet zone, which leads to uneven film edges on larger substrates. Note whether the liquid feed uses a syringe pump or a pressurized reservoir; the latter often drifts as the tank level drops, shifting the droplet size distribution mid-run.
Temperature control is another place where builds diverge. A hot plate with a single embedded thermocouple can read 400 °C while the substrate surface sits 60 °C lower because of air gaps and thermal mass differences. Ask for a thermal map, not a setpoint. Also compare the exhaust path: if the mist is pulled too aggressively across the substrate, you will see thinning along the leading edge. A slower, more diffuse extraction keeps the aerosol residence time more uniform.
Finally, think about how easy it is to clean and swap parts after a run. Ultrasonic nozzles clog with precursor salts, and some builds require removing four different fittings just to flush the tip. The checklist should include downtime between runs, not just deposition rate. If a vendor cannot show you a five-minute teardown of the spray head, that complexity will eventually show up in your repeatability data.
FAQ
Sono-Tek and Ultrasonic Systems, Inc. tend to come up most often, but Holmarc Opto-Mechatronics and Siansonic also have loyal users in university labs. MTI Corporation is worth a look if you need a more budget-conscious setup without giving up basic uniform coating capability.
It usually comes down to nozzle durability, droplet size consistency, and how well the liquid delivery path resists corrosion. A brand that offers clear maintenance documentation and responsive support also saves a lot of headaches when working with reactive precursors.
The nozzle sets the droplet size distribution and deposition velocity. A well-designed ultrasonic nozzle prevents pooling and clogging, which directly affects how smooth and dense the final thin film turns out, especially over larger substrate areas.
Yes. Sono-Tek's ExactaCoat series is often used in academic labs, and Holmarc offers tabletop spray pyrolysis units that fit under a standard fume hood. These smaller systems still include heated substrate stages and basic programmable controls.
Most use titanium or PTFE-coated fluid pathways, stainless steel nozzle bodies, and an optional inert gas shroud. That combination keeps the mist focused and prevents acid or solvent damage to internal seals over repeated runs.
In many cases, yes, but you need to adjust the substrate holder and grounding. Conductive substrates often require a stable back contact and uniform heating, while non-conductive materials may need a thin adhesion layer or surface plasma treatment to get reliable film nucleation.
Expect to flush the liquid line after each session with a compatible solvent, inspect O-rings and ultrasonic generator calibration monthly, and replace the nozzle tip when the spray pattern starts to show uneven edges. Those small habits can extend the system's life well beyond the warranty period.
Conclusion
In thin-film coating, trusting an ultrasonic spray pyrolysis system starts with uniform film quality, not glossy brochures. A few brands consistently deliver repeatable thickness across large areas because they obsess over nozzle geometry—orifice diameter, vibration frequency, and liquid feed stability all shape droplet size and distribution. Before committing, users should examine the nozzle closely and ask how the system handles viscosity changes, clogging, and solvent evaporation at the tip. The quiet engineering details often separate dependable builds from fragile ones: precise temperature control around the atomization zone, stable carrier gas flow, and effective transducer cooling keep a run steady for hours without drift. Real users also check whether the mist plume stays narrow and whether the exhaust path prevents recirculation onto already coated layers.
Where thin-film demands push hardest—dense perovskite layers, ultra-thin conductive oxides, or high-aspect-ratio surface coverage—weaker systems reveal themselves quickly through pinholes, edge buildup, or poor adhesion. Trustworthy suppliers tend to share failure data openly, offer spare piezoelectric elements, and agree to run a sample using the actual precursor chemistry rather than plain water. A practical comparison checklist helps: confirm the ultrasonic generator matches the nozzle’s resonance under load, ask about maintenance intervals for the transducer, and inspect whether the build is modular enough to adjust flow paths and substrate heating without voiding support. Brands that survive this scrutiny usually rely on user feedback loops and long-term field reports instead of vague performance claims. Ultimately, trust is earned through consistent film morphology, minimal overspray, and a supplier who responds honestly when parameters fall outside the manual’s comfort zone.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/