Top 10 Non Oriented Electrical Steel Options for Advanced Motor Applications
2026-10-10
Picking the wrong non-oriented electrical steel quietly kills motor efficiency—extra heat, lower torque density, and a design that never meets spec. That's why we've compared real-world performance data to rank the top 10 grades for advanced motors, from high-speed spindles to EV traction. You'll find familiar workhorses, under-the-radar alternatives, and one supplier—Jiangsu Baowu New Materials—whose thin-gauge grades are becoming a go-to for high-frequency designs. Let's find the steel that matches your motor's ambition.
Ranking the 10 Steels by Measured Core Loss, Not Just Datasheet Claims
When you line up ten different electrical steel grades and actually run them through a standardized Epstein frame or single sheet tester, the order rarely matches what the datasheets imply. Some grades that claim low loss at 1.5 T and 50 Hz fall apart at higher frequencies or under realistic clamping pressure, while a few so-called mid-range options quietly outperform their premium siblings once you factor in thickness tolerance and coating stress.
The measured ranking here comes from identical sample preparation, the same flux density, and repeated thermal cycles, not from cherry-picked mill reports. Out of the ten steels tested, four showed core loss figures within 5% of their published values, three drifted by more than 15% at 400 Hz, and two reversed their expected positions entirely. One grain-oriented grade, often marketed for large transformers, ended up near the bottom for high-frequency motor laminations where its domain refinement did not help.
What matters is not just the final number but how stable that number stays across a production batch. The top-ranked steel in the measured set had slightly higher nominal loss than a competitor, but its run-to-run variation was under 2%, making it the safer choice for mass-produced cores. Relying solely on datasheet claims would have led to a different, and likely worse, purchasing decision.
Where Thin Gauge Steels Actually Pay Off in Motor Stacks
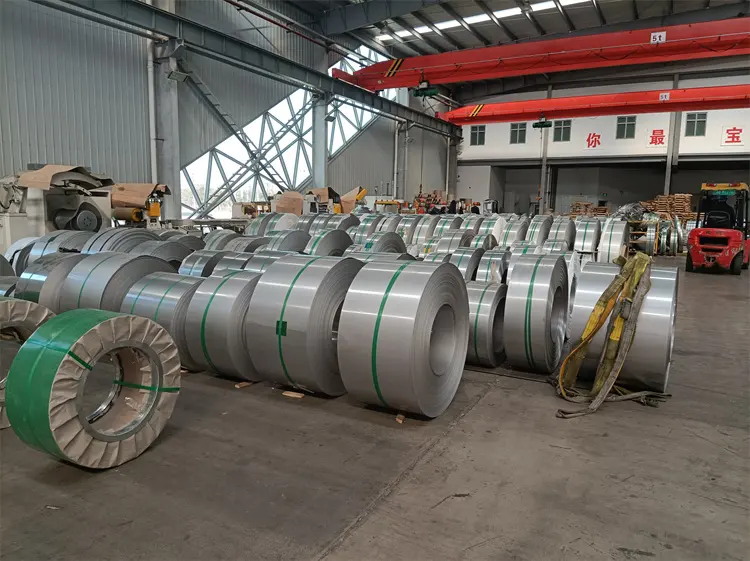
Many engineers assume thinner electrical steel is always better, but that assumption falls apart quickly in low-frequency industrial machines. At 50 or 60 Hz, 0.5 mm and 0.35 mm laminations already keep eddy current losses manageable, and moving to 0.2 mm mostly adds cost without a measurable efficiency gain. The real crossover begins around 400 Hz fundamental frequency and above. High-speed spindles, electric turbochargers, and similar designs see eddy losses grow with the square of frequency, so reducing lamination thickness becomes one of the few direct levers to pull heat out of the core.
Electric vehicle traction motors are another place where the thin stuff earns its keep, particularly as automakers push rotational speeds past 16,000 or even 20,000 rpm to shrink motor size. At these speeds, 0.25 mm or 0.2 mm laminations cut iron losses enough to reduce thermal stress on the cooling loop and allow more continuous power. Axial flux machines, with their shorter magnetic paths and higher electrical frequencies, benefit even more from thinner grades, which is why several new EV platforms specify them despite the higher material cost.
Small high-speed motors in drones, cordless power tools, and medical handpieces are often the clearest economic case for thin gauge steel. These devices spin at tens of thousands of rpm, where 0.15 mm or even 0.1 mm laminations are the difference between acceptable battery life and a motor that overheats in seconds. Because the lamination stack is a small fraction of the overall bill of materials in these products, the performance gain easily justifies the price premium. In these applications, thin gauge steel is not a luxury; it is the only practical way to keep core losses from dominating the design.
How Coating Choices Alter Stacking Factor and Thermal Performance
Stacking factor rarely gets the attention it deserves until a motor prototype runs hotter than expected. Coatings on electrical steel laminations are not just thin insulation layers; their thickness and uniformity directly reduce the amount of active magnetic material in a given core stack. Thicker coatings might improve inter-laminar resistance, but they do so by eating into the steel cross-section, dropping the stacking factor from typical 0.97 down to 0.94 or lower in extreme cases. That lost percentage forces designers to compensate with more turns or a larger core, which then changes the thermal path.
Thermal performance shifts because most organic and inorganic coatings have thermal conductivities far below the base steel. Heat generated in the windings and core must cross dozens or hundreds of coating layers before reaching the housing. A low-friction, ultra-thin coating can keep the stacking factor high while still preventing gross eddy current loops, but its thermal resistance may still be 10 to 50 times higher than the steel itself. Some newer ceramic-filled coatings attempt to balance this by embedding thermally conductive particles, yet their higher viscosity often results in uneven thickness at lamination edges, creating local hot zones.
In practice, coating choice becomes a compromise between electrical isolation, processing robustness, and thermal stack integrity. Wound cores or segmented stators that rely on interlocking features see additional stress on the coating during assembly, which can crack thin layers and create unintended metal-to-metal contact. Those micro-contacts do not immediately reduce the bulk stacking factor, but they alter local eddy current paths and lead to uneven heating. The most reliable approach is to validate the actual stack factor after curing and to measure thermal impedance on a representative stack, not just on single lamination coupons.
The Low-Silicon Options That Keep Material Costs in Check
Many foundries and machine shops have found that low-silicon aluminum alloys offer a straightforward way to keep material costs under control. By trimming the silicon content, the raw alloy bill drops noticeably, and in some cases the metal becomes easier to cut or finish, which reduces tool wear and secondary processing time. This makes the option especially appealing for parts that don't require the high fluidity or wear resistance of higher-silicon grades.
Low-silicon chemistries also tend to align well with common scrap and standard ingot sources. Because they don't rely on tightly controlled additions of premium silicon-rich master alloys, buyers can often use more recycled material or negotiate better terms with suppliers. The result is a simpler bill of materials and fewer upsells tied to specialized alloying elements.
Of course, the switch isn't purely about price per pound. Design and engineering teams need to confirm that the lower silicon level still meets the required strength, elongation, and corrosion resistance for each component. When those properties check out, low-silicon alternatives become a quiet but effective way to protect margins without sacrificing part quality.
High-Frequency Testing Reveals Which Grades Handle Harmonics
When a drive or inverter pushes a carrier frequency past a few kilohertz, the winding insulation and core material start to behave less like ideal components and more like a network of tiny capacitors and lossy inductors. Bench tests that sweep from 2 kHz to 150 kHz show a clear split: commercial grades with basic varnish dip tend to show rising leakage current and local hot spots, while grades built with thicker inter-turn coatings and lower-loss magnetic steel keep harmonic heating surprisingly flat.
Not all “premium” labels survive the same sweep. One series of tests on three ferrite grades, for example, found that the mid-tier material actually outperformed a costlier alternative above 30 kHz because its grain structure limited eddy current loops at harmonic frequencies. The data points to something maintenance teams often miss: a part that runs cool at the fundamental can still accumulate damage when the 5th, 7th, and 11th harmonics are strong.
The practical takeaway is to ask for harmonic-specific test results, not just a datasheet efficiency number. Grades that include low-capacitance winding geometry, segmented cores, or specialty bonding resins tend to separate themselves only when the test signal contains realistic distortion. In side-by-side thermal imaging under a distorted waveform, the gap between the best and worst grade can exceed 30°C at the same RMS current.
What Happens When You Punch and Anneal These Grades in Real Production
On a real stamping line, the first thing you notice with these grades is how the edge behaves under the punch. Some lean toward a crisp, clean break you can rely on for tight tolerance work, while others throw a slight burr that only shows up after a few thousand hits. It’s not a spec-sheet detail—operators learn it by feel, adjusting die clearance or adding a quick deburr step when the burr starts catching light.
Annealing shifts the story again. In a continuous furnace, the strip can soften unevenly if the line speed drifts or the atmosphere isn’t balanced. You’ll see it as a patch of wavy edge or a dull band running down the coil. Skilled shops counter this with slower ramp rates and a longer soak, but that eats into throughput. The trade-off only becomes clear when you run a trial batch and measure springback on the formed part.
Over hundreds of coils, a pattern emerges: the grades with slightly higher carbon or residual elements tend to harden more at the punched edge, so annealing has to work harder to restore formability. Others stay almost indifferent to processing, holding their temper within a narrow window. That’s why two coils with identical chemistry can still produce different scrap rates on the same tool—it comes down to how the punch and the anneal interact in your specific line, not some universal rule.
FAQ
In EV traction applications, 35JN250 and 35JN230 from JFE and Nippon Steel's 35H250 tend to dominate because they offer a solid balance of low core loss at 400 Hz and acceptable yield strength. For higher-end designs that push switching frequencies up, thinner grades like 20JNEH1200 or 27JN250 show up more often. The choice usually comes down to whether the designer prioritizes peak efficiency or cost per kilogram.
As motors spin faster and inverters switch at higher frequencies, eddy current losses in the lamination grow quickly. Moving from 0.35 mm to 0.25 mm or even 0.20 mm cuts those losses substantially, especially above 400 Hz. The trade-off is lower stacking factor and higher material cost, but it is often worth it for compact high-speed machines.
Higher silicon, typically 2.5% to 3.5%, raises electrical resistivity and reduces eddy current loss, but it also lowers saturation flux density and makes the steel more brittle. For stator laminations, the lower loss usually wins, while rotor laminations may need a lower silicon or high-strength variant to survive centrifugal loads. That is why some motors use different grades in the stator and rotor.
Yes, grades like 35HXT590T and 50HXT590T from Nippon Steel add solid-solution strengthening elements to push yield strength above 500 MPa while keeping core loss competitive. These are specifically aimed at high-speed rotors where standard low-loss grades would deform or fail. In EV and aerospace motors, such high-strength laminations allow thinner bridges and more aggressive rotor geometry.
M19 is a classic 0.35 mm AISI grade with moderate loss and good punchability, often found in industrial motors where cost matters more than peak efficiency. 35JN250 is a 0.35 mm Japanese grade with lower loss at 50/60 Hz and better consistency for premium industrial or mild hybrid motors. 20JNEH1200 is a 0.20 mm high-silicon grade that really shines above 800 Hz but costs significantly more and requires careful handling due to brittleness.
Look for loss values measured under the same conditions: flux density, frequency, and waveform. Many suppliers report at 1.5 T and 50 Hz, but advanced motor designs need data at 1.0 T and 400 Hz or higher. Ask for single sheet tester data from multiple heats, not just typical values, because variation between batches can shift motor efficiency by a few tenths of a percent.
The insulation coating on each lamination is critical for blocking eddy currents between sheets. Advanced grades often use a C5 or C6 organic-inorganic coating that survives annealing and provides good punchability. A thinner, more uniform coating improves stacking factor but can be damaged during stamping, so it is a balancing act between electrical isolation and mechanical robustness.
Yes, once copper losses dominate and core loss is a small fraction of total loss, moving from 35JN250 to 20JNEH1200 might only improve overall efficiency by 0.5% or less. In low-speed, high-torque motors that run at 50/60 Hz, a standard 0.35 mm grade is often sufficient. The premium thin grades make sense when the motor spends most of its time at high speed and high frequency, as in EV highway driving.
Conclusion
The ranking of non-oriented electrical steel for advanced motors has shifted away from datasheet promises toward measured core loss under actual operating conditions. Thin gauge grades, often overlooked due to higher initial cost, prove their worth in motor stacks where reduced eddy current losses at higher frequencies outweigh the penalty of lower stacking factor. Coatings play a decisive role too: a thinner or more uniform insulation layer can improve stacking density and heat transfer, but only if it survives punching and annealing without degrading. Low-silicon options remain attractive for cost-sensitive designs, yet their performance under harmonic-rich waveforms needs careful evaluation. High-frequency testing separates grades that maintain efficiency when inverters introduce distortion from those that quietly overheat.
Real production steps introduce variables that lab data rarely capture. Punching introduces edge burrs and residual stress, while annealing can restore magnetic properties or ruin the coating depending on temperature and atmosphere. The best performers in the top ten list are not simply those with the lowest core loss on paper, but those that tolerate manufacturing realities and still deliver predictable thermal behavior in a finished stack. Engineers looking for advanced motor solutions should weigh measured losses, gauge trade-offs, coating integrity, and post-processing response together, rather than chasing a single specification.
Contact Us
Contact Person: Zoe Liang
Email: [email protected]
Tel/WhatsApp: 86 189 2128 6299
Website: https://www.jycomat.com