Sanitary Pad Making Machine Manufacturer: Advanced Production Solutions
2026-09-23
Every minute, millions of sanitary pads roll off production lines—but too many manufacturers still struggle with downtime, material waste, and inconsistent quality. If your line is falling behind, advanced production technology isn't a luxury; it's the difference between leading the market and chasing it. Womeng builds next-generation sanitary pad making machines around one goal: turning raw materials into finished products with minimal waste and maximum uptime. Here's what smart manufacturing looks like when every second and every gram counts.
How High-Speed Lines Keep Unit Costs Low Without Sacrificing Absorbency
Running a high-speed production line often triggers worries about quality slipping as output climbs. The assumption is that faster machines mean thinner materials, rushed bonding, or uneven fiber distribution. Yet modern lines flip this logic: they use precision control systems and real-time feedback loops to hold absorbency steady while throughput soars. Operators tune the forming head and vacuum levels so the fluff pulp settles densely where it matters most, without dumping extra raw material across the whole sheet. That targeted approach keeps the per-unit fiber cost from ballooning, even as the line cranks out thousands more pieces per hour.
The real savings come from waste reduction, not from shaving material off every product. High-speed equipment catches defects earlier with inline vision systems, so rejected batches shrink from a few per hour to a handful per shift. Changeover times drop too, since automated guides and quick-release tooling let crews swap formats in minutes instead of stopping for half an hour. Those minutes add up across a year, and they don't touch the core absorbency spec at all. In fact, some lines recover trim waste and feed it back into the process, lowering raw input cost while keeping the final product's performance identical to slower, older machines.
Energy efficiency plays a quieter but equally important role. Faster lines spread fixed overhead like heating, compressed air, and operator wages across more units, so the cost per item falls naturally. Smart motor drives and heat exchangers capture waste from drying sections, reducing the kilowatt-hours per ton of output. None of those changes require a lighter basis weight or weaker absorbent core; they simply use the same material more intelligently. As a result, buyers get the same soak-up capacity they expect, while the plant sees unit economics that make low-margin products viable at scale.
Material Handling Systems That Prevent Delamination and Glue Bleed
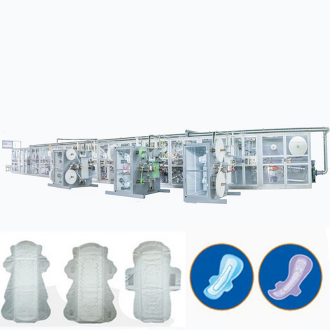
Delamination and glue bleed rarely start with the adhesive itself. More often they show up when stacked panels shift during transport, when a vacuum head applies unequal suction across a freshly bonded surface, or when conveyor rollers create tiny shear forces at the edge of a still-soft glue line. A well-designed material handling system treats every transfer point as a potential stress riser. It avoids hard stops, keeps acceleration ramps smooth, and maintains panel alignment from layup through final cure.
On the floor, this translates into a few specific choices. Vacuum lifters with individually controlled zones can hold a full sheet without pulling unevenly on one corner. Transfer conveyors that use tight roller spacing and synchronized belt speeds prevent the subtle slipping that squeezes adhesive out along the edges. Where panels must be stacked before full cure, racks with load-spreading pressure pads and gentle indexing motions keep each layer in place without introducing lateral movement.
Some of the most effective systems also integrate short dwell stations or cooling tunnels before stacking. Giving the glue line fifteen to thirty seconds under controlled airflow lets the outer edge tack up enough to resist bleed when weight is applied. Paired with sensors that flag misaligned edges or excessive clamp pressure, these handling steps reduce rework far more reliably than simply increasing adhesive cure time.
The Role of Modular Tooling in Quick Product Changeovers
Traditional dedicated tooling often turns a simple product switch into a drawn-out battle with bolts, shims, and trial-and-error alignment. Modular tooling flips that script by breaking the setup into interchangeable, pre-aligned building blocks. Instead of tearing down an entire fixture, operators swap only the product-specific elements while the base plate stays locked in place. That alone can cut changeover time from hours down to minutes, freeing machines for actual production instead of idle recalibration.
The real advantage comes from standardizing interfaces. When every modular component uses the same locating pins, quick-release clamps, and preset stop positions, there is no need for skilled technicians to re-indicate each job. Offline presetting becomes routine: a new product's tooling is assembled and measured away from the machine, then rolled in and clamped down with repeatable accuracy. This shifts setup work from a bottleneck on the line to a parallel activity, so the next job is ready before the current one even finishes.
Beyond speed, modular systems reduce human error and make changeovers predictable. Color-coded plates, foolproof docking features, and clearly marked torque points allow less experienced operators to perform swaps confidently. Companies also gain flexibility to reconfigure tooling for low-volume runs or prototype work without investing in another full set of dedicated fixtures. In high-mix production environments, that adaptability often matters more than raw speed, because it lets a single machine serve many product variants without sacrificing uptime or quality.
Why Servo-Driven Cutting Outperforms Traditional Rotary Dies
Traditional rotary dies rely on mechanical cams and gear trains to synchronize the cutting motion with the web speed. This works fine at a constant velocity, but the moment you speed up, slow down, or switch to a thinner material, the fixed geometry starts to introduce small variations in cut length. Servo-driven systems replace that entire mechanical linkage with an electronic cam profile that tracks the actual web position in real time. The result is a cut that stays accurate within a few hundredths of a millimeter, even during rapid acceleration or deceleration. You can change the cut length on the fly without stopping the line, and the servo automatically compensates for material stretch or slip that would otherwise cause rejects.
Another place where servo cutting pulls ahead is in handling short runs or frequent product changeovers. A conventional rotary die needs a new die set and often a different gear ratio to shift from one cut length to another. That means downtime, manual adjustment, and a pile of dedicated tooling for every SKU. A servo-driven cutter uses the same cutting head but simply loads a new motion profile. Operators can dial in a new length from the HMI, and the machine is ready in seconds. For packaging converters running twenty or thirty different pouch sizes in a single day, that flexibility translates directly into more productive hours on the floor.
Durability and maintenance also tell a clear story. Mechanical rotary dies experience high shock loads every time the blade strikes the anvil, which leads to wear on bearings, gears, and the die itself. Servo systems smooth out that impact by controlling the velocity profile of the blade at the moment of contact. The motor can decelerate slightly just before the cut, then accelerate away, reducing peak forces on the entire assembly. Over months of continuous operation, this translates into fewer unexpected breakdowns, longer blade life, and a more consistent cut edge—without the constant fiddling that mechanical systems often demand.
Built-In Quality Checks That Catch Defects Before Packaging
At each critical assembly station, high-speed cameras and laser profilometers compare the part against its reference model, flagging dimensional drift, surface blemishes, or misplaced components within milliseconds. A deviation of just a few microns can stop the line and route the unit to a rework bay, so defects never accumulate downstream.
For products with moving parts or electrical contacts, automated test rigs run a scripted sequence that mirrors real-world abuse: buttons are pressed hundreds of times, connectors are mated and unmated, and current draw is monitored for microamp-level anomalies. Every single unit goes through this gauntlet, not a random sample, which makes late-stage failures rare.
Right before packaging, a final checkpoint verifies weight, scans barcodes and label text, and checks seal integrity where applicable. If an accessory is missing or a label is smudged, the system diverts the item to a side queue and logs the exact failure reason, giving operators immediate visibility into the root cause.
After-Sales Support That Goes Beyond Spare Parts
When a machine goes down, the real question isn't whether you can find a replacement part—it's whether anyone will help you understand why it failed in the first place. Our support team treats every service call as a diagnostic puzzle, not a warehouse transaction. You won't just get a box with a new component; you'll get a technician who walks through the failure timeline with your crew, checks related stress points, and suggests adjustments that could prevent the same issue from recurring next month.
That's why we've moved our after-sales engineers into the field, not just behind a phone queue. They carry the same torque wrenches and thermal imagers your maintenance team uses, and they're trained to spot wear patterns before they become breakdowns. After a repair, expect a follow-up visit—not a survey email—where we measure vibration, temperature, and alignment while the equipment is under real load. If something looks off, we'll fix it on the spot, often without an invoice.
Beyond the hardware, you get access to a living support portal where your specific machine's service history, modification notes, and predictive maintenance alerts are updated in real time by the people who actually turned the wrenches. No generic FAQ pages, no ticket number roulette. Just practical guidance from technicians who know your line as well as you do, and who treat a 2 a.m. breakdown call like an invitation to earn your next purchase.
FAQ
The line handles ultra-thin, maxi, night, and panty liner formats through interchangeable forming modules, letting you switch profiles in under thirty minutes without replacing the entire core assembly.
Servo-driven indexing and closed-loop tension control keep each layer aligned, while inline vision inspection catches wrinkles or shifted cores before they reach the sealing station.
Yes, the unwinding and hot-melt systems are calibrated for bamboo fiber, organic cotton, and plant-based backsheet films, with temperature zones adjusted to avoid heat damage on sensitive substrates.
Most projects move from floor-leveling to first commercial output in four to six weeks, including operator training on recipe management, size changeovers, and daily maintenance routines.
Each adhesive station uses independent metering pumps and multi-nozzle patterns with real-time flow monitoring, so coating weight stays within a narrow band even during acceleration or deceleration phases.
Absolutely, quick-change size parts and servo-adjustable guides allow you to run different lengths, widths, and fold styles, while the packaging module can handle pillow packs, flow wraps, or carton-ready bundles.
You get remote diagnostics around the clock, regional spare-part hubs for critical wear items, and on-site engineers who can be dispatched within 48 hours for mechanical or control system faults.
Automated splicing aligns the new roll edge, precise cut-off knives retract during thread-up, and edge trim is pulled into a reclaim system rather than dropping to the floor, cutting scrap by roughly a third compared to manual setups.
Conclusion
A modern sanitary pad manufacturing line succeeds only when speed, material integrity, and flexibility work together. High-speed production keeps unit costs low, but the real engineering challenge lies in maintaining absorbency at elevated throughput. Advanced manufacturers achieve this by precisely controlling fiber opening, core formation, and compression, so the pad retains its fluid lock even when output climbs. Material handling systems play an equally critical role: poorly managed tension or adhesive application leads to delamination and glue bleed, which ruin both performance and appearance. Through closed-loop tension control and low-temperature adhesive systems, these machines keep each layer bonded cleanly from unwind to final cut. Modular tooling then adds commercial agility, allowing a quick switch between pad lengths, shapes, or absorbency levels with minimal downtime. Instead of dedicating separate lines to different SKUs, converters reconfigure forming drums, cutting units, and sealing modules in a matter of hours.
The cutting and inspection stages determine how much of that precision actually reaches the consumer. Servo-driven cutting outperforms traditional rotary dies because it synchronizes blade position with web speed in real time, eliminating edge drift, ragged cuts, and unnecessary material waste. This becomes especially valuable when running thin cores or printed backsheets, where even a millimeter of misalignment is visible. Built-in quality checks then close the loop: high-resolution vision systems and pressure sensors inspect pad thickness, placement of wings, and seal integrity before packaging, so defective units are rejected upstream rather than reaching the carton. Finally, after-sales support extends beyond spare parts. The best manufacturers provide remote performance monitoring, on-site process audits, and operator training programs that help converters fine-tune tension, temperature, and servo parameters. This ongoing collaboration keeps line efficiency high as raw material batches and product designs evolve, making advanced production solutions a long-term asset rather than a one-time purchase.
Contact Us
Contact Person: Jessie Lai
Email: [email protected]
Tel/WhatsApp: 86-188594442931
Website: https://www.wm-machinery.com