Reliable Oil Flow Switch What to Look For Before You Buy
2026-11-16
Most oil flow switch failures aren't sudden—they're slow, intermittent, and expensive. A switch that trips too late lets a compressor starve for lubrication; one that trips too often shuts down a line for no reason. Reliability doesn't come from a brand name on the housing. It comes from matching the switch to the actual flow range, oil viscosity, temperature swings, and electrical load. Buy the wrong spec and you're not fixing a problem—you're installing the next service call. Before you place an order, know what separates a five-year switch from a five-week one. If you want a line built for real operating conditions rather than a lab bench, HONGSEN is a good place to start.
Switch Point Accuracy You Can Actually Verify
Factory tolerances often make printed actuation distances feel like suggestions rather than facts. With magnetic or Hall effect switches, the trigger point is determined by a sensor reading the magnet's position, so you can set it to 0.5mm, 1.2mm, 2.0mm and then test whether the key actually fires at that depth. The difference becomes obvious the moment you stop relying on a spec sheet and start measuring with a simple USB protocol analyzer or a dedicated switch tester.
A practical check takes a few minutes. Set the actuation point in the keyboard's software, then press the key slowly while watching the live travel readout. On a well-tuned board, the switch registers exactly when the on-screen travel distance crosses the line you set. If the reading jumps from 0.8mm to 1.1mm with no in-between values, the sensor resolution or firmware smoothing is hiding real inaccuracy. Repeat the test on all keys—edge keys near the case tend to show more deviation because of slight magnet alignment differences.
What separates a board you can trust from one that just claims precision is consistency across the whole deck. A good implementation keeps every switch within ±0.1mm of the target point after calibration. You can verify this by exporting the raw sensor data or using the keyboard's own diagnostic mode, if it has one. If the manufacturer doesn't give you a way to see per-key travel data, treat any advertised accuracy number as marketing until proven otherwise.
Can the Wetted Materials Survive Your Oil Chemistry?
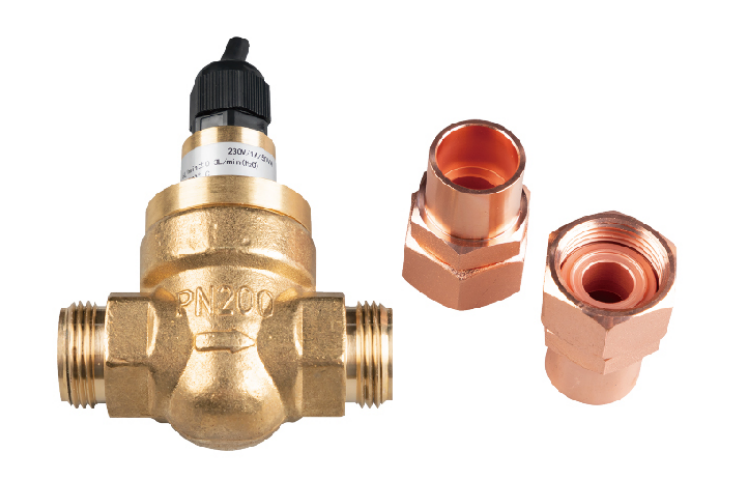
The first thing to check is whether the seals, gaskets, and internal coatings actually hold up when they come into contact with your specific oil blend. Many standard elastomers look fine on a spec sheet but start swelling, cracking, or losing elasticity once additives like esters or high-pressure agents get involved. A simple soak test at operating temperature often reveals failures that a generic compatibility chart misses.
Beyond the obvious softening or hardening, pay attention to subtle changes in surface roughness and tensile strength over time. Some materials absorb a small percentage of oil weight and still perform fine, while others leach plasticizers that contaminate the fluid itself. If your oil contains aggressive detergents or metal deactivators, even a “chemical-resistant” polymer might degrade faster than expected under continuous flow conditions.
The most reliable approach is to run a side-by-side comparison using actual field samples rather than relying on published resistance tables. Because oil chemistry varies with oxidation byproducts and top-up practices, what survives in a clean lab environment may fail after six months in a hot sump. Document any changes in durometer, volume, and visual appearance weekly, and treat borderline results as a warning sign for future leaks or particle shedding.
Flow Response Time and False Trigger Behavior
A flow switch that responds too slowly can turn a minor process hiccup into a larger problem. In systems where liquid starts and stops abruptly, the delay between actual flow change and switch output is often where nuisance alarms or missed cycles originate. Getting this timing right isn’t just about matching a datasheet value; it depends on pipe diameter, media viscosity, and how far the sensor sits from bends or pumps. Even a 200-millisecond lag can matter when a booster pump needs to shut off before a dry-run condition develops.
False triggers, on the other hand, usually come from turbulence or transient pressure spikes rather than genuine flow reversals. A paddle-style sensor mounted too close to an elbow may bounce with eddies and send a “flow present” signal even when the main stream has stopped. Likewise, air pockets passing a thermal dispersion probe can briefly cool the sensing element and mimic a sudden flow loss. Filtering or damping helps, but over-filtering slows response and reintroduces the first problem. The practical sweet spot is often found by testing under worst-case startup and shutdown conditions, not just steady-state flow.
Electrical Output Compatibility Beyond the Datasheet
Engineers often treat the datasheet as the final word on electrical output, but real-world systems rarely behave like the lab bench where those numbers were captured. Output voltage tolerances, current limits, and transient response are typically specified under narrow conditions—fixed input, room temperature, resistive load. Once you add cable inductance, varying supply rails, or capacitive loads, the actual output can drift far from the nominal curve. A 5V rail may sag to 4.6V under a fast load step, or a current-limited supply may enter hiccup mode unexpectedly. Understanding these deviations requires measuring behavior across the full operating envelope, not just reading the headline specs.
One common trap is assuming that the output remains stable under any load the datasheet claims as “supported.” For instance, a regulator rated for 1A continuous might oscillate when connected to a low-ESR ceramic capacitor bank without the recommended series resistance. Another overlooked area is cross-regulation in multi-output converters: loading one rail heavily can cause the other to rise beyond its specified tolerance, even if both are within their individual limits on paper. These effects are not always documented, but they surface quickly in field returns or EMC test failures.
To design beyond the datasheet, prototype with realistic parasitics and worst-case load patterns. Add intentional margin for output capacitance and ESR, and verify stability with a network analyzer or load-step test. For high-reliability applications, consider derating the output current by 20–30% if the ambient temperature exceeds the datasheet’s test condition. The goal is not to distrust the manufacturer’s data, but to recognize that every electrical output lives in a system—and that system writes its own spec once power meets PCB trace.
Installation Constraints from Pipe Size to Orientation
The diameter of the pipe often dictates how much room you need for elbows, flanges, and valve actuators, especially when the line runs close to a wall or ceiling. A modest 2-inch line can snake through a chase with minimal clearance, but once you step up to 8-inch or larger, the turning radius alone can force you to shift support brackets, relocate access panels, or even reroute adjacent conduit. What looks straightforward on a schematic becomes a tight puzzle when the physical hardware and wrench swing space are taken into account.
Orientation adds another layer of practical constraint that pipe size alone does not capture. A vertical riser may require guide supports at shorter intervals than a horizontal run of the same diameter, while a sloped drain line must maintain its grade without being shoved out of alignment by a nearby beam or duct. In tight mechanical rooms, flipping a valve from horizontal to vertical can mean the difference between a clean installation and one where the handle collides with a structural column or blocks a required egress path.
Beyond the static fit, think about how size and orientation interact with thermal expansion and vibration. A long horizontal run of large-diameter pipe will move noticeably when heated, so anchors and expansion loops need room that is often overlooked during initial layout. Similarly, a vertical drop that feeds a pump should not be so tall that the weight strains the pump casing or so short that the inlet becomes air-bound. These are not code-driven limits you can look up in a table; they come from walking the route, measuring the actual clearances, and respecting how the pipe will behave after it is filled and put into service.
Long-Term Stability and Maintenance Access
Long-term stability often gets reduced to a single uptime percentage, but the real test is whether a system continues to behave predictably as dependencies shift and traffic patterns evolve. Maintenance access plays a quietly central role here: without a well-governed path for engineers to inspect logs, apply patches, or adjust configuration, even the most robust initial design will drift into a fragile state. The goal is not simply to keep the service running, but to ensure that every future intervention—whether planned or emergency—can happen without introducing new failure modes.
The tension around maintenance access usually emerges from two competing fears. Locking things down too tightly might prevent a quick fix during an incident, while leaving doors open invites accidental changes or security gaps. In practice, the most stable long-running systems tend to treat access as a living set of permissions rather than a static decision. Teams that routinely audit who can do what, and under which conditions, find that their maintenance windows become shorter and less disruptive—not because access is restricted, but because it is understood.
A less obvious factor is how maintenance access affects the people involved. When engineers know they can safely investigate a slowdown or apply a minor version bump without jumping through excessive hoops, they are more likely to perform proactive upkeep. Conversely, if every change requires a formal request that takes days, small issues accumulate until they become large ones. Stability, then, is as much about the confidence to act as it is about the technical safeguards. The best access models make routine maintenance feel unremarkable, which in turn keeps the system from becoming a museum piece that nobody dares to touch.
FAQ
A switch should be matched to your system's actual flow velocity and oil viscosity, not just the pipe diameter. For thin turbine oils, a paddle-style unit rated around 0.5–3 m/s often works, but thicker gear oils may need a larger paddle or a different sensing principle to avoid sticking.
Yes, especially the seals and paddle. Some elastomers swell or harden in contact with certain oil additives or high temperatures. Brass or stainless steel bodies are generally safe, but always verify that O-rings and diaphragms are made from Viton, EPDM, or another material compatible with your specific oil.
Never size a flow switch for just the normal operating pressure. Pump startups, quick valve closures, or clogged filters can create spikes well above steady state. Choose a housing rated for at least 1.5 times your maximum expected surge pressure to avoid cracked fittings or blown seals.
Not always. Many paddle-type switches are designed for horizontal pipes with the paddle hanging downward. If you must install in a vertical line or with upward flow, look for a model that explicitly supports that orientation, or consider a thermal or inline shuttle-type switch instead.
Mechanical reed switches or relays are fine for occasional alarm duty, but they can wear out if the switch cycles frequently. For high-cycle applications or PLC inputs, a solid-state output lasts longer and avoids contact bounce. Just make sure the output rating matches the load you are switching.
Usually yes. A simple LED or mechanical flag lets operators confirm flow without opening a control panel or checking a remote display. During commissioning, it is also a quick way to verify that the switch trips at the right point, which can save hours of troubleshooting.
An adjustable time delay or damping feature is your best defense. A 2–5 second delay lets the switch ignore brief air pockets or flow fluctuations during pump priming, while still tripping on a true loss of flow.
For hazardous areas, ATEX, IECEx, or UL/CSA certification must match the zone and gas group. Even in a clean plant, an IP65 or IP67 housing is worth specifying for dust, moisture, or washdown exposure.
Conclusion
Buying an oil flow switch that holds up over time starts with two questions most datasheets gloss over: can you verify the switch point in your actual system, and will the wetted parts tolerate your specific oil chemistry? Look for designs that let you confirm the set point under real flow conditions rather than relying on a factory calibration that may drift or never match your viscosity. At the same time, check every material that touches the oil—O-rings, paddle, body, and float—against additives, water content, and temperature swings. A switch that works fine in light hydraulic oil can swell, crack, or bind in a different formulation, so don't assume "oil-compatible" means your oil.
Beyond that, pay attention to response time and false trigger behavior, especially if your system starts and stops frequently or has pulsating flow. A switch that chatters or needs a long delay to change state can cause nuisance alarms or missed low-flow events. Then confirm the electrical output actually matches your control panel—not just the voltage and current ratings, but also whether the switch provides a dry contact, NPN/PNP, or analog signal, and how it behaves during power loss. Finally, think through installation constraints like pipe size, required straight run, and orientation limits, and ask how you'll access the unit for cleaning or calibration a year from now. Long-term stability in oil service often depends on accessible, field-serviceable parts rather than a sealed throwaway design.
Contact Us
Contact Person: KOPASS HO
Email: [email protected]
Tel/WhatsApp: 8613606566112
Website: https://www.hongsenref.com/