High Quality Air Bubble Detector Guide for Reliable Fluid Monitoring
2026-09-30
Few failures in fluid handling are as silent and consequential as an undetected air bubble. Whether you're running a dialysis machine, a bioreactor, or a high-precision dispensing system, even a micro-bubble can skew results, damage equipment, or put patients at risk. That's why selecting the right air bubble detector isn't just a checkbox—it's a critical design decision. In this guide, we break down what makes a high-quality detector, from sensing technology to response time, and show how Siansonic solutions fit into reliable fluid monitoring setups.
Why Bubble Size and Flow Rate Matter More Than You Think
Most people assume that any bubble stream works the same, but the physical dimensions of each bubble and the speed at which they're released change everything about how the water moves. A tiny bubble rises slowly and lingers near the surface, while a larger one pushes upward with more force and creates a wider column of circulation. This difference isn't just cosmetic—it directly affects how oxygen gets mixed into the tank, how waste particles are pushed toward the filter, and whether your fish experience gentle currents or stressful turbulence.
Flow rate, often overlooked, acts as the hidden variable that either amplifies or cancels out the benefit of bubble size. Too slow, and even perfectly sized bubbles fail to create meaningful water turnover. Too fast, and the bubbles merge into unstable slugs that rattle the surface and splash beyond the rim. The sweet spot sits where each bubble remains distinct yet travels fast enough to drag surrounding water along with it. That balance is what turns a decorative bubbler into a functional part of your aquarium's life support.
When you adjust both factors together, the results are immediate and measurable. A finer bubble diffuser running at a moderate flow can lift detritus from plant leaves without uprooting them, while a coarser stone at the same flow merely agitates the top layer. Likewise, a high-flow pump paired with small bubbles can strip CO2 too quickly for planted tanks, whereas the same pump with larger bubbles might be ideal for a bare-bottom breeding setup. Paying attention to these two details lets you fine-tune the invisible engine that keeps your water clear and your livestock calm.
The Hidden Costs of Ignoring Air in Peristaltic Pump Lines
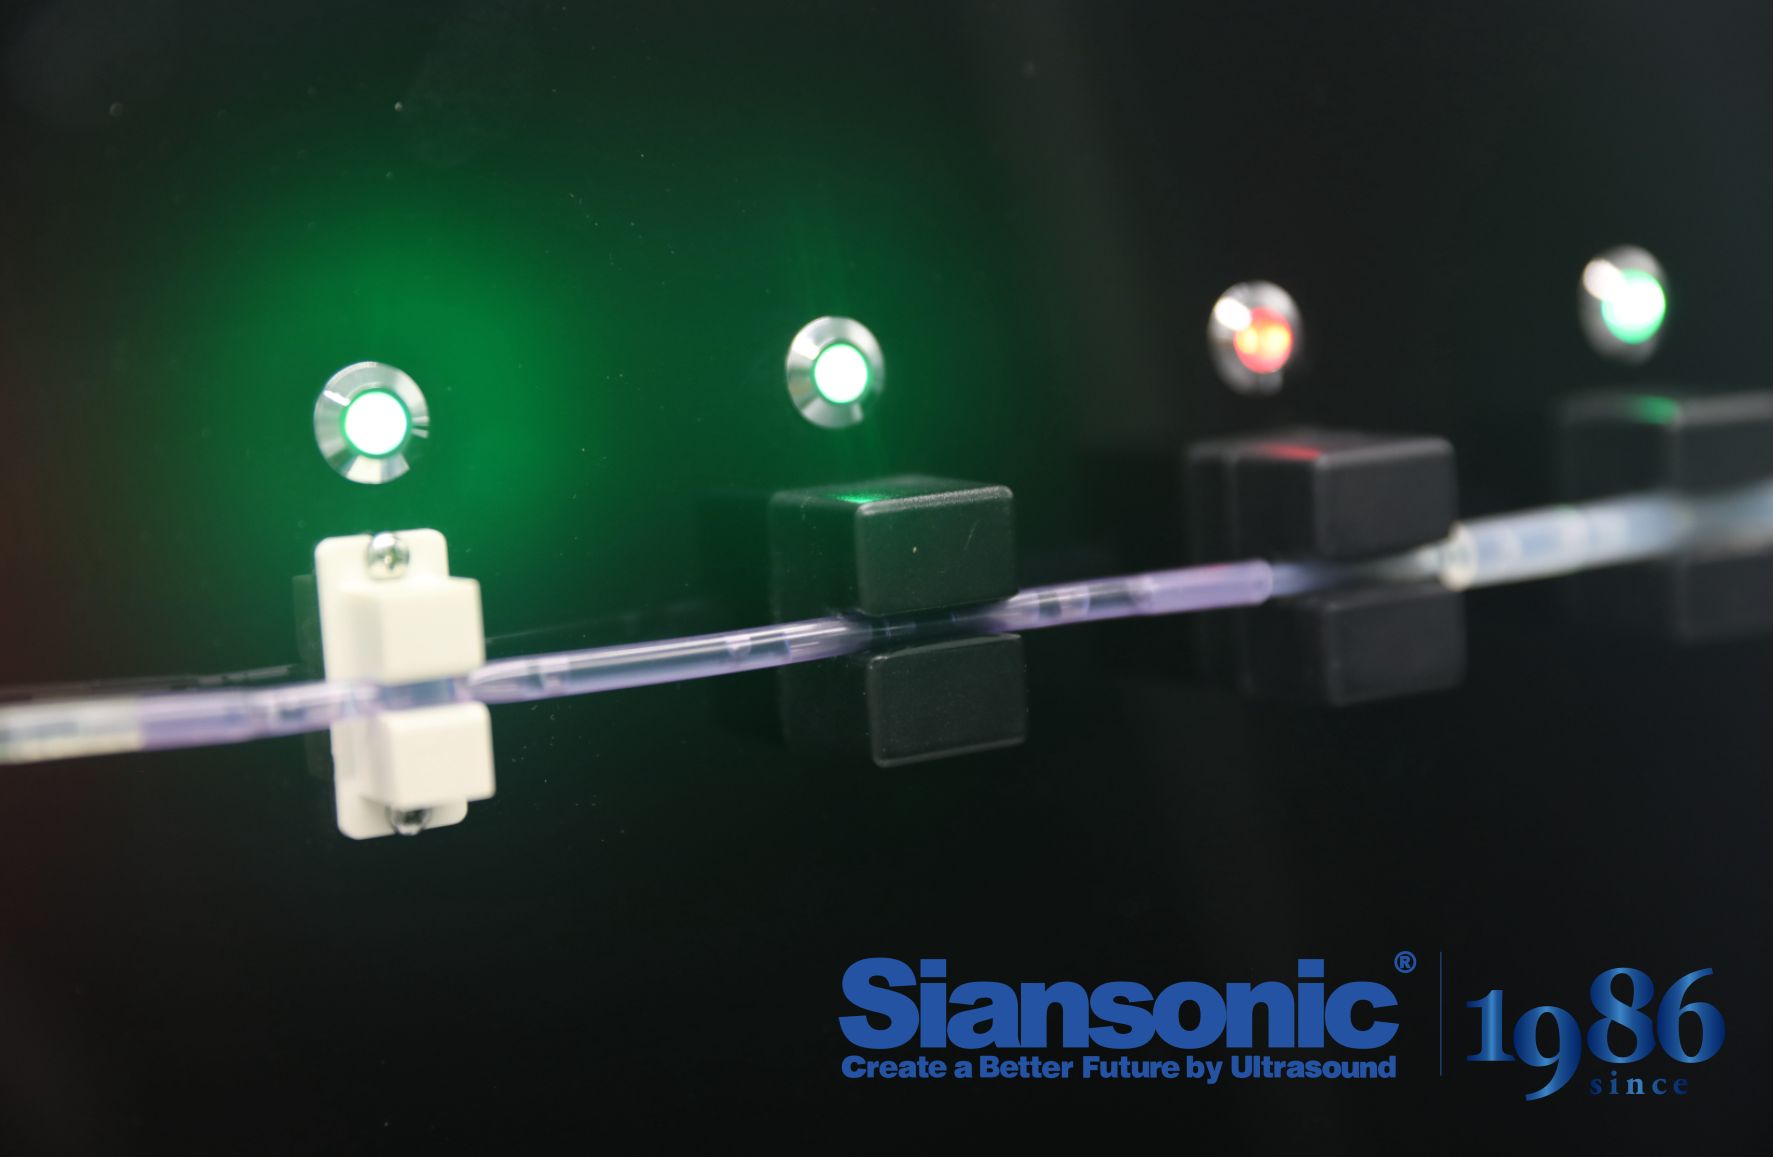
When air sneaks into peristaltic pump lines, it rarely triggers an immediate alarm. The real damage shows up later: dosing inconsistencies, premature tube wear, and a slow drift in process accuracy that operations teams end up chasing for weeks. A bubble trapped near a check valve might reduce each stroke's delivered volume by a few percent—not enough to fail a single batch, but plenty to compromise cumulative results.
The financial sting compounds quietly. Maintenance crews replace tubing more often because air pockets create uneven compression and localized fatigue. Sensors drift out of calibration as they try to compensate for erratic flow, leading to overcorrection and wasted reagents. Then there's the labor cost of troubleshooting "phantom" issues—technicians disassemble lines, run diagnostics, and find nothing obviously wrong because the air has already moved downstream.
Ignoring air in the lines also shortens the life of downstream components. Filters clog faster when air bubbles cause turbulent flow and particle resuspension. Diaphragms and seals degrade from repeated micro-hammer effects. By the time the root cause is identified, the accumulated expenses in replacement parts, overtime, and lost production often dwarf the cost of a proper debubbling or priming procedure.
Sensor Placement Tricks That Cut False Alarms by Half
Most false alarms come down to one thing: the sensor is looking at the wrong thing. Start by mapping where people, pets, and moving shadows actually cross—not just where the manual says to mount. A sensor aimed at a stairwell's top step will catch far fewer phantom triggers than one staring down a hallway that catches every passing cat.
Height and angle matter more than sensitivity settings. Mounting a PIR sensor at chest height instead of ceiling height changes its detection cone from a wide blanket to a narrow slice, which means a blowing curtain or a hot air vent stops looking like an intruder. If you can, shim the bracket a few degrees downward so the beam ends at the floor instead of hitting a reflective window.
Walk the space after installation and act like a false alarm: wave a jacket near a vent, walk past at the edge of the room, place a cardboard box in a sunny spot for an hour. If the sensor trips on these, it will trip at 3 a.m. Move it before you trust it.
How to Pick Between Ultrasonic and Optical Detection Without Guesswork
Choosing between ultrasonic and optical detection usually comes down to what’s actually in your environment, not a spec sheet. If you’re dealing with dusty, smoky, or humid conditions, ultrasonic sensors tend to be more forgiving because sound waves don’t care about airborne particles. Optical sensors, on the other hand, can get thrown off by steam, fog, or even a bright reflection from a nearby surface. Before you commit, walk the actual space and note what’s floating around or shining in the background.
Another practical distinction is how each technology handles odd-shaped targets. Ultrasonic waves bounce back from almost any solid object, whether it’s clear glass, a dark plastic bin, or a rough cardboard box. Optical detection—especially laser-based or reflective types—often struggles with transparent, shiny, or very dark materials. If your application has variety in what’s moving past the sensor, lean ultrasonic unless you’re willing to tune and test each target.
Mounting distance and speed of response also separate the two. Ultrasonic sensors work well for longer ranges and slower cycles, but they have a dead zone close to the face and can be sluggish if objects appear and disappear quickly. Optical sensors excel at fast, precise detection at shorter distances, which makes them the default pick for high-speed packaging or counting tasks. Ask yourself how fast the process really moves—and whether a few milliseconds of lag will cause a jam.
A Field Guide to Calibrating Detectors for Viscous or Opaque Fluids
Calibration starts with a simple concession: the fluid will not cooperate with optical alignment tools or tidy lab standards. For viscous oils, pastes, or slurries, bring the detector to the fluid's working temperature before any baseline reading. A cold honey-like sample will give you drift that looks like sensor error but is really just viscosity changing with each degree. Let the loop circulate for at least twenty minutes, then verify with a handheld viscometer or a timed cup measurement rather than trusting the detector's internal temperature probe.
Opaque fluids remove your ability to see bubbles, sediment, or coating on the sensor face. Work blind but not careless. Use an in-line reference cell with a known calibration fluid of similar refractive index or acoustic impedance, depending on the detector type. For ultrasonic or optical detectors, a short bypass loop lets you switch between process fluid and reference fluid without tearing down the line. Record the raw signal, not just the scaled output; factory scaling often assumes clear water and becomes meaningless in black liquor or heavy crude.
Finally, do not chase a perfect zero. In viscous or opaque service, a stable offset is more valuable than a clean baseline. After adjusting gain and damping, run three short batches with differing flow rates—or different fill levels if it is a level detector—and compare the detector's trend against a manual grab sample. If the offset repeats within your tolerance, lock it in and document the temperature and pressure at calibration. That field note will save you more time than any vendor manual.
Real-World Cases Where Bubble Detectors Prevented Catastrophic Contamination
At a sterile fill-finish line for injectable oncology drugs, a peristaltic pump began drawing air through a hairline crack in a silicone tubing segment. The inline bubble detector, positioned just before the filling needles, registered a 0.5 mL air bolus within 200 milliseconds and sent a stop signal to the filling manifold. Vials already on the line were automatically rejected, and the batch was paused. A subsequent inspection showed that the crack had developed only minutes earlier; without the detector, air would have displaced liquid drug product in several hundred vials, creating a sterility breach that could have led to patient infections and a full market recall.
In a semiconductor fab, a chemical delivery system supplying photoresist to a track tool began to outgas due to a failing degassing membrane. The bubble detector installed downstream of the pressure vessel detected microbubbles as small as 2 µL in the resist stream and immediately closed the dispense valve. This prevented the spray of resist mixed with gas from reaching the wafer surface, where it would have caused comet-shaped defects and scattered organic contamination across the coating chamber. The tool was taken offline, the membrane replaced, and no wafers were lost.
A biopharmaceutical chromatography skid processing a monoclonal antibody was recirculating buffer through a Protein A column when a loose sanitary fitting allowed air to enter the low-pressure side. The ultrasonic bubble sensor on the feed line detected a slug of air 30 seconds before the column inlet. The control system diverted the feed to waste and initiated a column re-equilibration cycle. Because the air never reached the packed bed, the antibody load was protected from channeling and endotoxin contamination that would have required discarding the entire 200-liter batch.
FAQ
It spots unwanted gas pockets in liquid lines and triggers an alarm or stops the pump before those bubbles reach sensitive downstream components. Think of it as an early warning system that prevents dosing errors, sensor damage, or product contamination.
Ultrasonic models work well with opaque or viscous fluids where light can't pass through. Optical detectors are ideal for clear tubing and low-cost setups. Capacitive sensors handle non-conductive liquids but can drift with temperature. Match the sensing principle to your tubing material and fluid properties, not just the price.
Place it at a point where bubbles are most likely to form or collect, usually right after a pump, valve, or degassing chamber. Avoid mounting it on a curve or right next to a vibrating motor, because both can create false positives or missed events.
Rarely. Most detectors are tuned for a specific range of tube diameters and wall thicknesses. Silicone, PVC, and Tygon each affect acoustic or optical signals differently, so check the manufacturer's calibration chart. Using a detector outside its specified tube range is a common cause of unreliable readings.
Good units are mostly self-calibrating and need little more than an occasional wipe of the sensor window or coupling surface. I recommend a verification check every 6–12 months using a controlled injection of air or a reference obstruction, just to confirm the alarm threshold hasn't drifted.
Ignoring the flow rate specification. A detector that works perfectly at 50 mL/min may completely miss bubbles at 500 mL/min because the bubble passes the sensing zone faster than the response time. Always check the maximum flow velocity, not just the tube size.
Medical infusion and dialysis are the most well-known, but they also protect inkjet printers, semiconductor chemical delivery, food and beverage filling lines, and fuel cell systems. Any process where a gas pocket can ruin a batch or damage equipment is a candidate.
First, rule out electrical noise by separating signal cables from motor or heater wiring. Then check for micro-bubbles caused by outgassing or a loose fitting upstream. If both are clean, the issue is often an incorrect tube size or a bubble detector mounted too close to a pump pulsation source.
Conclusion
A bubble detector is only as good as its ability to match real flow dynamics. Bubble size and flow rate determine whether a sensor can catch a transient air pocket or a steady stream of microbubbles, so knowing your system's typical bubble profile is the first step toward reliable monitoring. In peristaltic pump lines, ignoring air isn't just a nuisance—it leads to dosing errors, reagent waste, and contaminated batches that quietly drain budgets. Smart sensor placement, such as positioning the detector at a slight downward angle or close to the pump outlet, reduces false alarms caused by turbulence or tubing flex, often cutting nuisance trips by half. Choosing between ultrasonic and optical detection isn't about brand preference; it's about fluid clarity, tubing material, and whether the liquid carries particulates that scatter light or absorb sound.
Calibration for viscous or opaque fluids demands more than a factory default. For high-viscosity media, you often need to slow the sample flow or use a wider tubing ID to let the acoustic or optical signal differentiate between a true air gap and a temporary void from cavitation. Real-world cases show bubble detectors preventing catastrophic contamination in cell culture harvests, dialysis machines, and pharmaceutical filling lines—where a single undetected air slug would have ruined an entire batch or endangered a patient. The guide's core takeaway: treat bubble detection as a system-level decision, not a component swap. Match the sensor physics to your fluid and line geometry, verify with your own bubble challenges rather than idealized test loops, and you'll get dependable air monitoring that quietly protects product quality and patient safety.
Contact Us
Contact Person: Ivy Zhang
Email: [email protected]
Tel/WhatsApp: +86 1081502288
Website: https://www.siansonic.com/