China Package Printing Die Making Equipment: Essential Buying Considerations
2026-10-07
Buying package printing die making equipment in China isn't just about finding the lowest quote. The real challenge is balancing precision, speed, and after-sales support—areas where many buyers get burned. If you're evaluating suppliers, you need a clear-eyed checklist. This guide covers the factors that actually impact your bottom line, from blade accuracy to machine rigidity. And when it comes to trusted manufacturing partners, ADEWO stands out for its engineering focus and transparent process. Let's dive into what you should look for before signing any contract.
Matching Machine Capabilities to Your Everyday Die Jobs
Before you slide a die into the press, take a minute to measure the shut height and compare it against the machine's adjustment range—not just the nominal daylight. Many everyday die jobs fail because the ram never reaches the right bottom position, or the bolster plate flexes under loads the tonnage rating alone doesn't reveal.
Stroke length matters more than it first appears. A short-stroke press can force a deep draw to be split across extra hits, while an overly long stroke on a simple blanking die wastes cycle time and adds unnecessary shock. Watch how the die behaves during the first few strokes and listen for uneven impacts; that feedback often shows whether the press's energy and speed are actually suited to the job.
Keep a simple log for each die and machine pairing. Note what adjustment you started with, where the ram ended up, and any slug pulling or part sticking that occurred. Over a few weeks, these notes turn into a practical range you can trust far more than a generic capacity chart.
Examining Build Quality Beyond the Polished Exterior
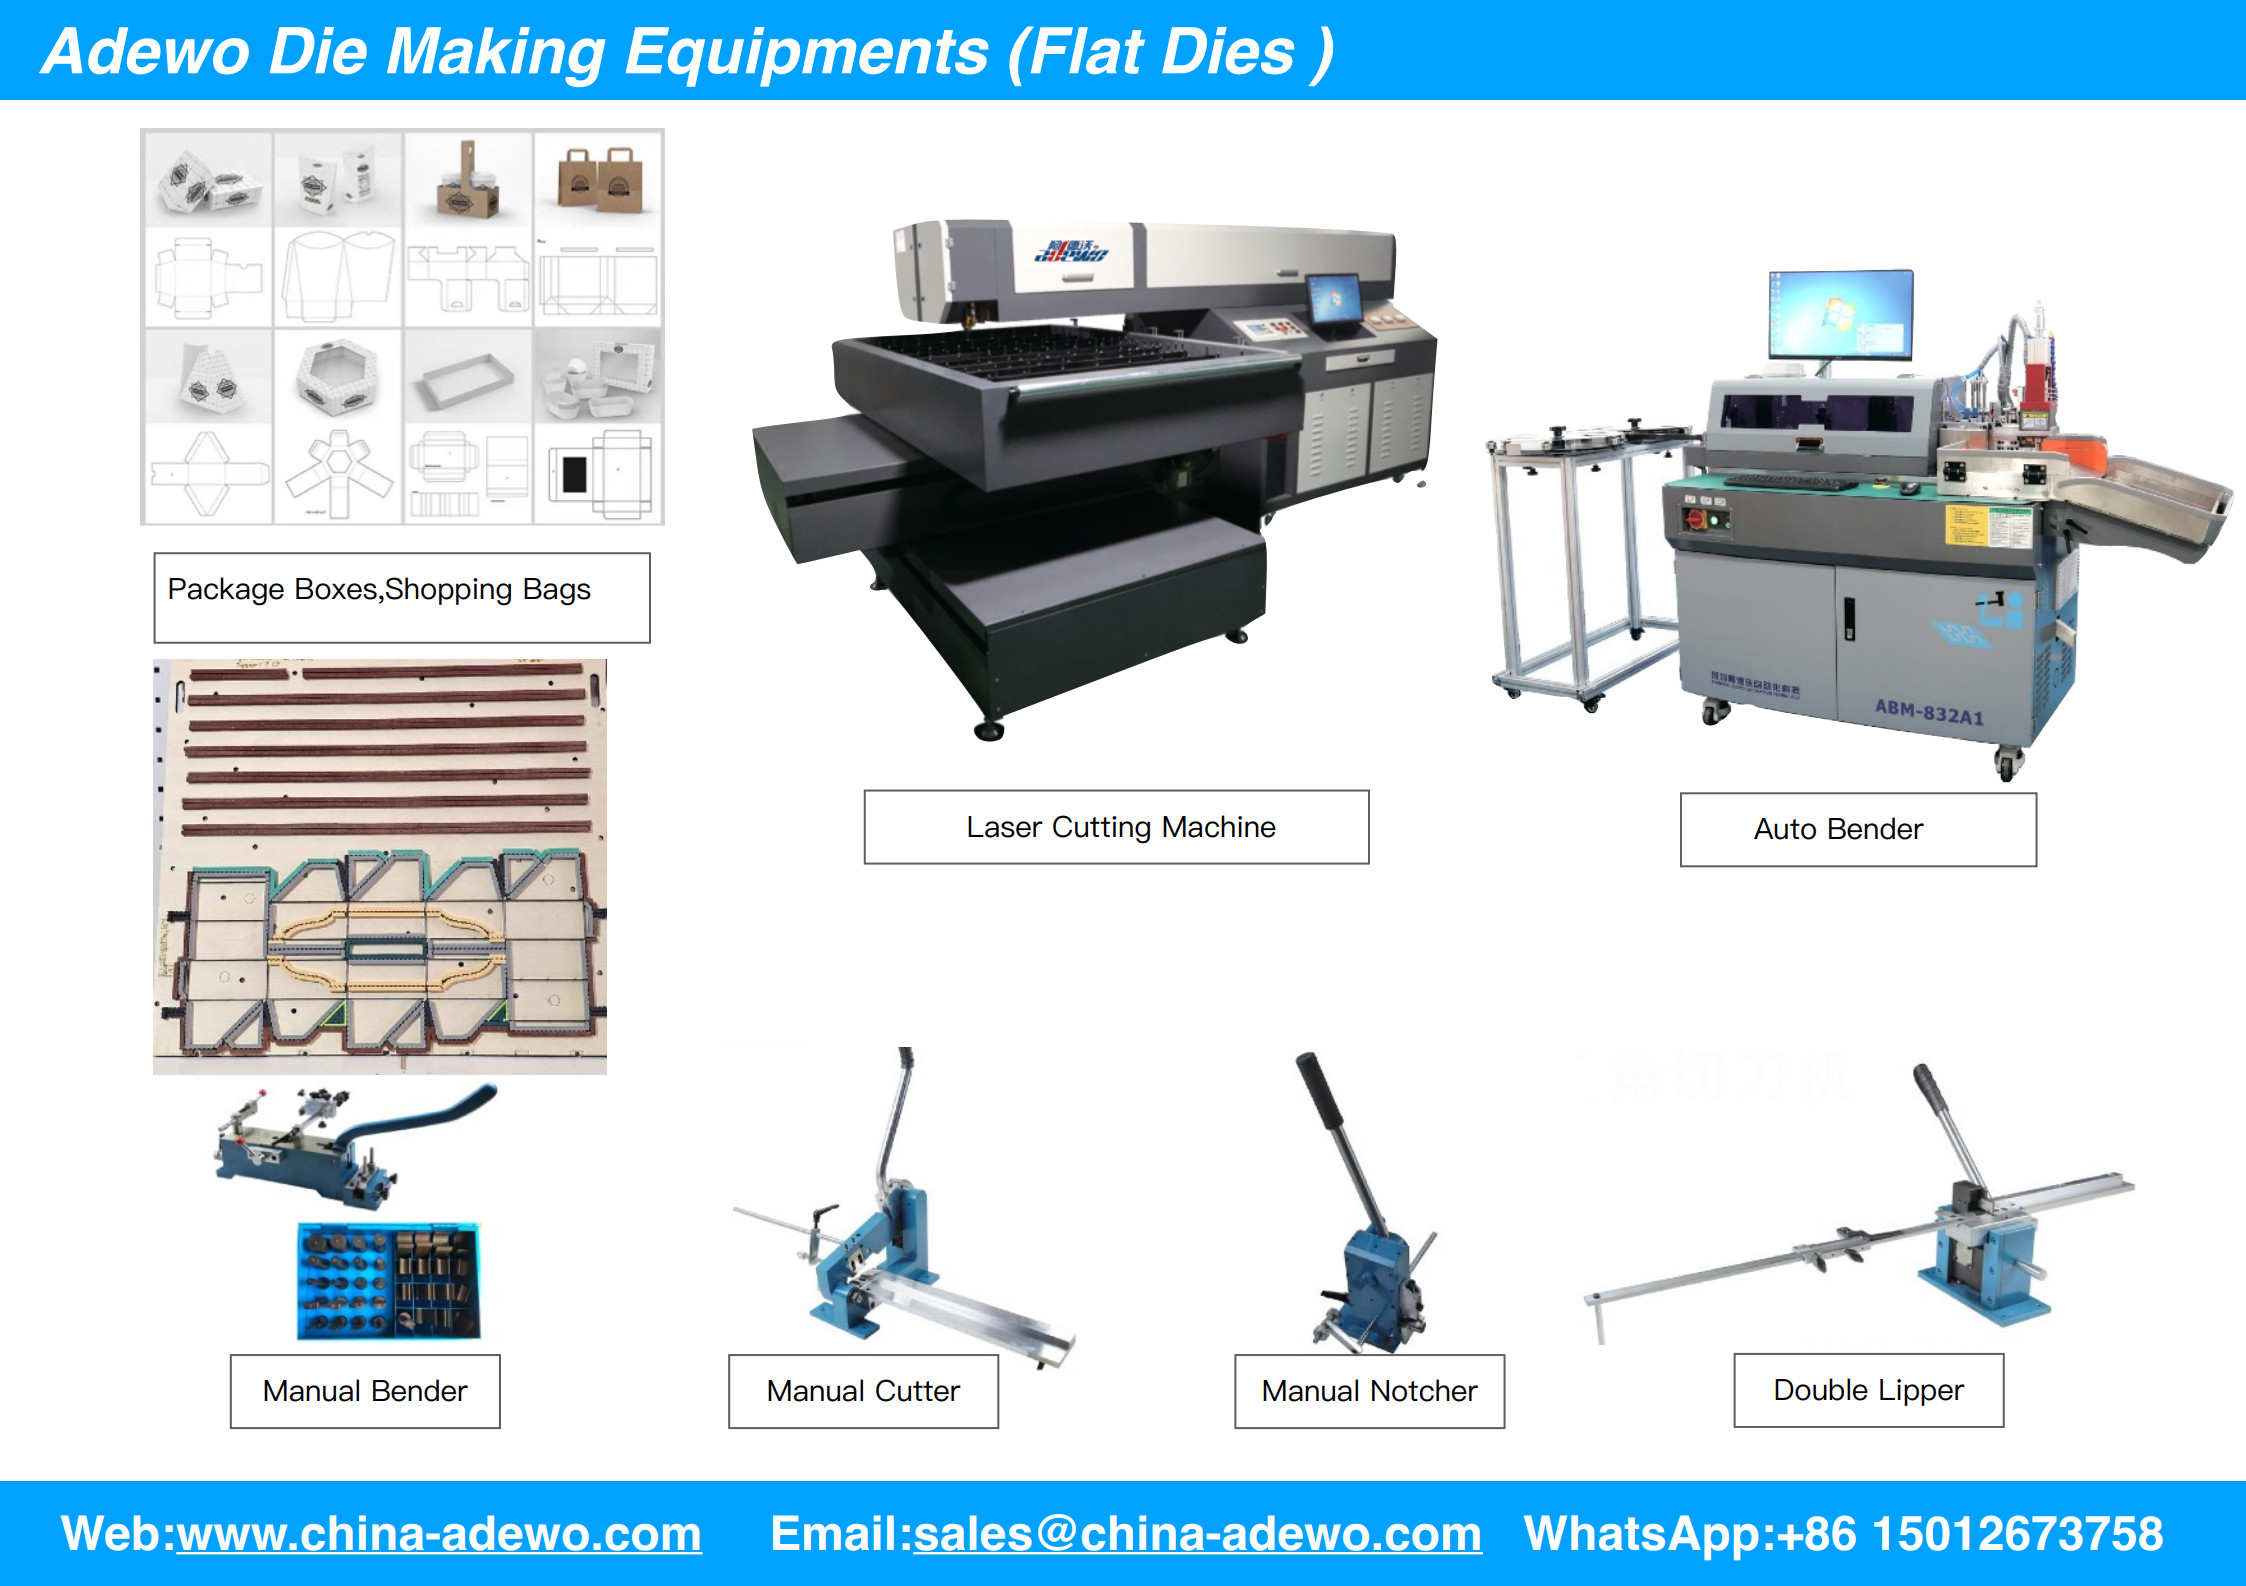
The first thing most people notice is the smooth finish or the sleek lines, but true build quality lives in the places you don't see on a showroom floor. Run your fingers along the inside edges of a drawer, check the weight distribution when you lift a corner, or listen to the sound a hinge makes after ten thousand cycles. These are the details that separate a product designed for longevity from one that simply looks good in a photograph. A well-built item should feel solid without being overly heavy, and its moving parts should operate with a quiet confidence—no wobble, no grinding, no unexpected flex.
Materials matter more than marketing. Solid wood versus veneer, forged aluminum versus stamped steel, double-stitched seams versus glued trim—each choice has consequences for how the product ages. Take a closer look at the joints: are they reinforced with dowels, brackets, or interlocking geometry, or do they rely on a thin bead of adhesive? Press firmly on load-bearing surfaces. If you feel any give or hear a faint creak, that's a warning sign. High-quality construction often reveals itself through subtle indicators like consistent gap widths, properly countersunk fasteners, and edges that are chamfered rather than left sharp.
Durability testing goes beyond the occasional tumble or spill. Think about thermal cycling if the item contains electronics, UV exposure for anything that lives near a window, or salt spray for metal components in coastal environments. A builder who cares about longevity will have considered these scenarios and chosen coatings, seals, and materials accordingly. The real test is time, but you can shortcut the process by examining how the product handles minor stress: flex a seam, toggle a switch, or load a shelf beyond its rated capacity for just a second. Genuine quality doesn't flinch under scrutiny.
Why Laser Power Alone Won't Guarantee Clean Cuts
It's tempting to think that more watts will slice through anything, but laser cutting doesn't work that way. Excess power often creates a wider heat-affected zone, leading to melted edges, stubborn dross, and occasional burn marks on thin materials. The real trick is matching power to material thickness and travel speed so the beam cuts through without lingering long enough to cause thermal damage.
Focus and beam quality frequently matter more than raw wattage. A tightly focused, lower-power beam can produce a narrower kerf and cleaner edge than a high-power beam with poor focus or a large spot size. Assist gas also plays a critical role: the right pressure and nozzle alignment blow molten material out of the cut. If the gas flow isn't dialed in, cranking up the power just leaves more slag clinging to the bottom edge.
Material properties add another layer. Highly reflective alloys or metals with high thermal conductivity can scatter or carry away heat so quickly that even a powerful beam struggles to make a clean entry. In those cases, adjusting pulse frequency, cutting speed, and gas type often delivers better results than simply pushing the power higher. A clean cut comes from balancing all these variables, not from wattage alone.
Understanding the True Availability of Local Service and Parts
Many equipment buyers assume that having a local dealer automatically means fast access to parts and skilled technicians. In practice, that dealer might only stock common consumables while everything else has to be ordered from a distant distribution center. Even a part listed as “available” online can be sitting in a warehouse hundreds of miles away, adding days or weeks to a critical repair. Without verifying the depth of local inventory and the training of the service staff, you could find yourself waiting on a single gasket or sensor while your operation grinds to a halt.
A better approach is to ask pointed questions before you commit. Request specific part numbers for the components most likely to fail and ask the dealer to show you the physical shelf stock, not just a computer screen. Check whether the local technicians have factory-level certifications for your exact model, and ask about typical response times for both phone support and on-site visits. Speaking with other local customers about their actual repair experiences often reveals gaps that brochures and sales presentations conveniently skip.
Accounting for Installation, Training, and Workflow Disruption
The price tag on new software rarely tells the whole story. Installation often feels straightforward until you realize your team's existing data needs cleaning, custom fields require mapping, and legacy systems resist every import attempt. Factor in the hours your IT staff spends untangling permissions or chasing down odd error messages, and the initial quote is already a distant memory.
Training is another line item that hides in plain sight. A vendor might offer a few onboarding videos, but your people don't learn by watching alone. They need hands-on practice, they ask questions that no FAQ covers, and some will stumble through the first month making mistakes that cost real money. Budget for a dedicated trainer or at least a power user who can hold informal workshops. Otherwise, you're paying for software that sits half-used while productivity dips.
Then there's the quiet killer: workflow disruption. Every time a department shifts from an old process to a new one, orders slow down, support tickets pile up, and managers burn hours putting out small fires. If you roll out the tool during a busy season, the disruption compounds. Smart buyers map out a slow transition period, keep old systems running in parallel for a while, and accept that the first quarter's efficiency numbers will look worse before they look better.
Choosing a Chinese Supplier With Genuine Package Printing Experience
Many buyers assume that any packaging factory in China can handle print jobs, but real expertise shows up in the fine details—ink adhesion on textured substrates, color consistency across large runs, and knowing which coating prevents scuffing during shipping. A supplier with genuine package printing experience will ask about your product's weight, shelf environment, and handling chain before quoting, rather than simply matching a Pantone number and hoping for the best.
One practical way to test this experience is to request printed samples on your actual material, not just digital proofs. Then look closely at registration accuracy on folded cartons, the depth of blacks on flexible film, and how the surface resists a thumbnail scratch. Factories that have spent years troubleshooting these issues will often send samples with a short note explaining what they adjusted—an indication that they see printing as a craft, not a commodity step.
Beyond the technical checks, ask how they handle artwork file preparation. A seasoned supplier will spot potential problems early: fonts that need outlining, barcode quiet zones that are too tight, or spot colors that would shift under a laminate. Their questions during the quotation stage reveal the depth of their printing background. If they treat artwork like a checklist item rather than a design conversation, you may end up paying for reprints instead of a reliable partnership.
FAQ
Look beyond the spec sheet and ask for actual cutting samples on the materials you use. Precision claims often fall apart on thin films or heavy board, so request a live demonstration or a trial run with your own stock before committing.
It's the foundation of long-term accuracy. A cast-iron frame with stress-relieved welding will hold tolerance far better than a lightweight fabricated base. Ask about heat treatment and vibration damping—cheap frames cause die wear and registration drift within months.
Not always. Many factories specialize in one type. If you need both, look for a builder that offers interchangeable workstations or has separate production lines for flatbed and rotary tooling. Hybrid machines exist but often compromise on speed or cutting depth.
This is often overlooked. Make sure the machine’s control system can import your CAD/CAM files directly, ideally supporting common formats like DXF, DWG, or AI. Some Chinese suppliers use proprietary software that adds conversion steps and hidden licensing costs.
Ask for the exact steel grade and hardness rating of the cutting rule or engraving tool. Reputable makers use D2, M2, or tungsten carbide and will share heat treatment records. If they refuse or give vague answers, walk away—cheap tooling will cost you far more in downtime.
For most buyers, a phased approach works best. Start with a CNC router or laser cutter plus a bending machine, then add a rule processor or inspection system as volume grows. Buying a full turnkey line can lock you into one supplier for all future upgrades.
Expect at least remote video support, but push for an on-site technician during installation. Also clarify spare parts lead times and whether they have a local distributor or service partner. Some companies offer very competitive prices but weak after-sales; check references from buyers in your region.
Request a video tour of their factory floor, not just marketing photos. Look for CNC machining centers, coordinate measuring machines, and a dedicated QC area. Ask how many machines they ship monthly and whether they have ISO 9001 or similar certification. If possible, hire a third-party inspection before shipment.
Conclusion
When evaluating die making equipment from China, start with the jobs that actually run through your shop. A machine that looks impressive in a brochure may struggle with the specific materials, thicknesses, and die sizes you handle daily, so match table size, cutting force, and repeatability to your typical work rather than chasing the highest spec sheet. Build quality often hides behind a shiny exterior: check frame rigidity, linear rail alignment, and the quality of drive components. A flimsy base or loose tolerances will show up as inconsistent die edges within months. Also remember that laser wattage alone is a poor predictor of cut quality. Beam mode, focus control, assist gas delivery, and motion system synchronization matter far more for clean cuts on wood, plastic, or steel rule bases. Some lower-wattage machines with superior optics and path planning outperform higher-wattage units that only burn through material.
The second half of the decision is less about the hardware and more about what happens after delivery. Before committing, verify the real availability of local service technicians and spare parts; a fast response promise from a sales office is not the same as a stocked parts warehouse or a technician within driving distance. Installation, operator training, and the inevitable workflow disruption during setup must be budgeted realistically, since a new die system can idle a packaging line for days if conversion is mishandled. Finally, seek out a Chinese supplier with genuine package printing experience, not just a general CNC builder. Ask for references from folding carton or corrugated converters, visit a running installation if possible, and look for a team that understands die registration, rule bending, and stripping pin placement. Suppliers rooted in packaging workflows will anticipate your problems instead of learning them on your floor.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com