Calcium Sulfate Six-Sided Steel-Faced Floor Manufacturer: Your Guide to Quality Access Floors
2026-09-09
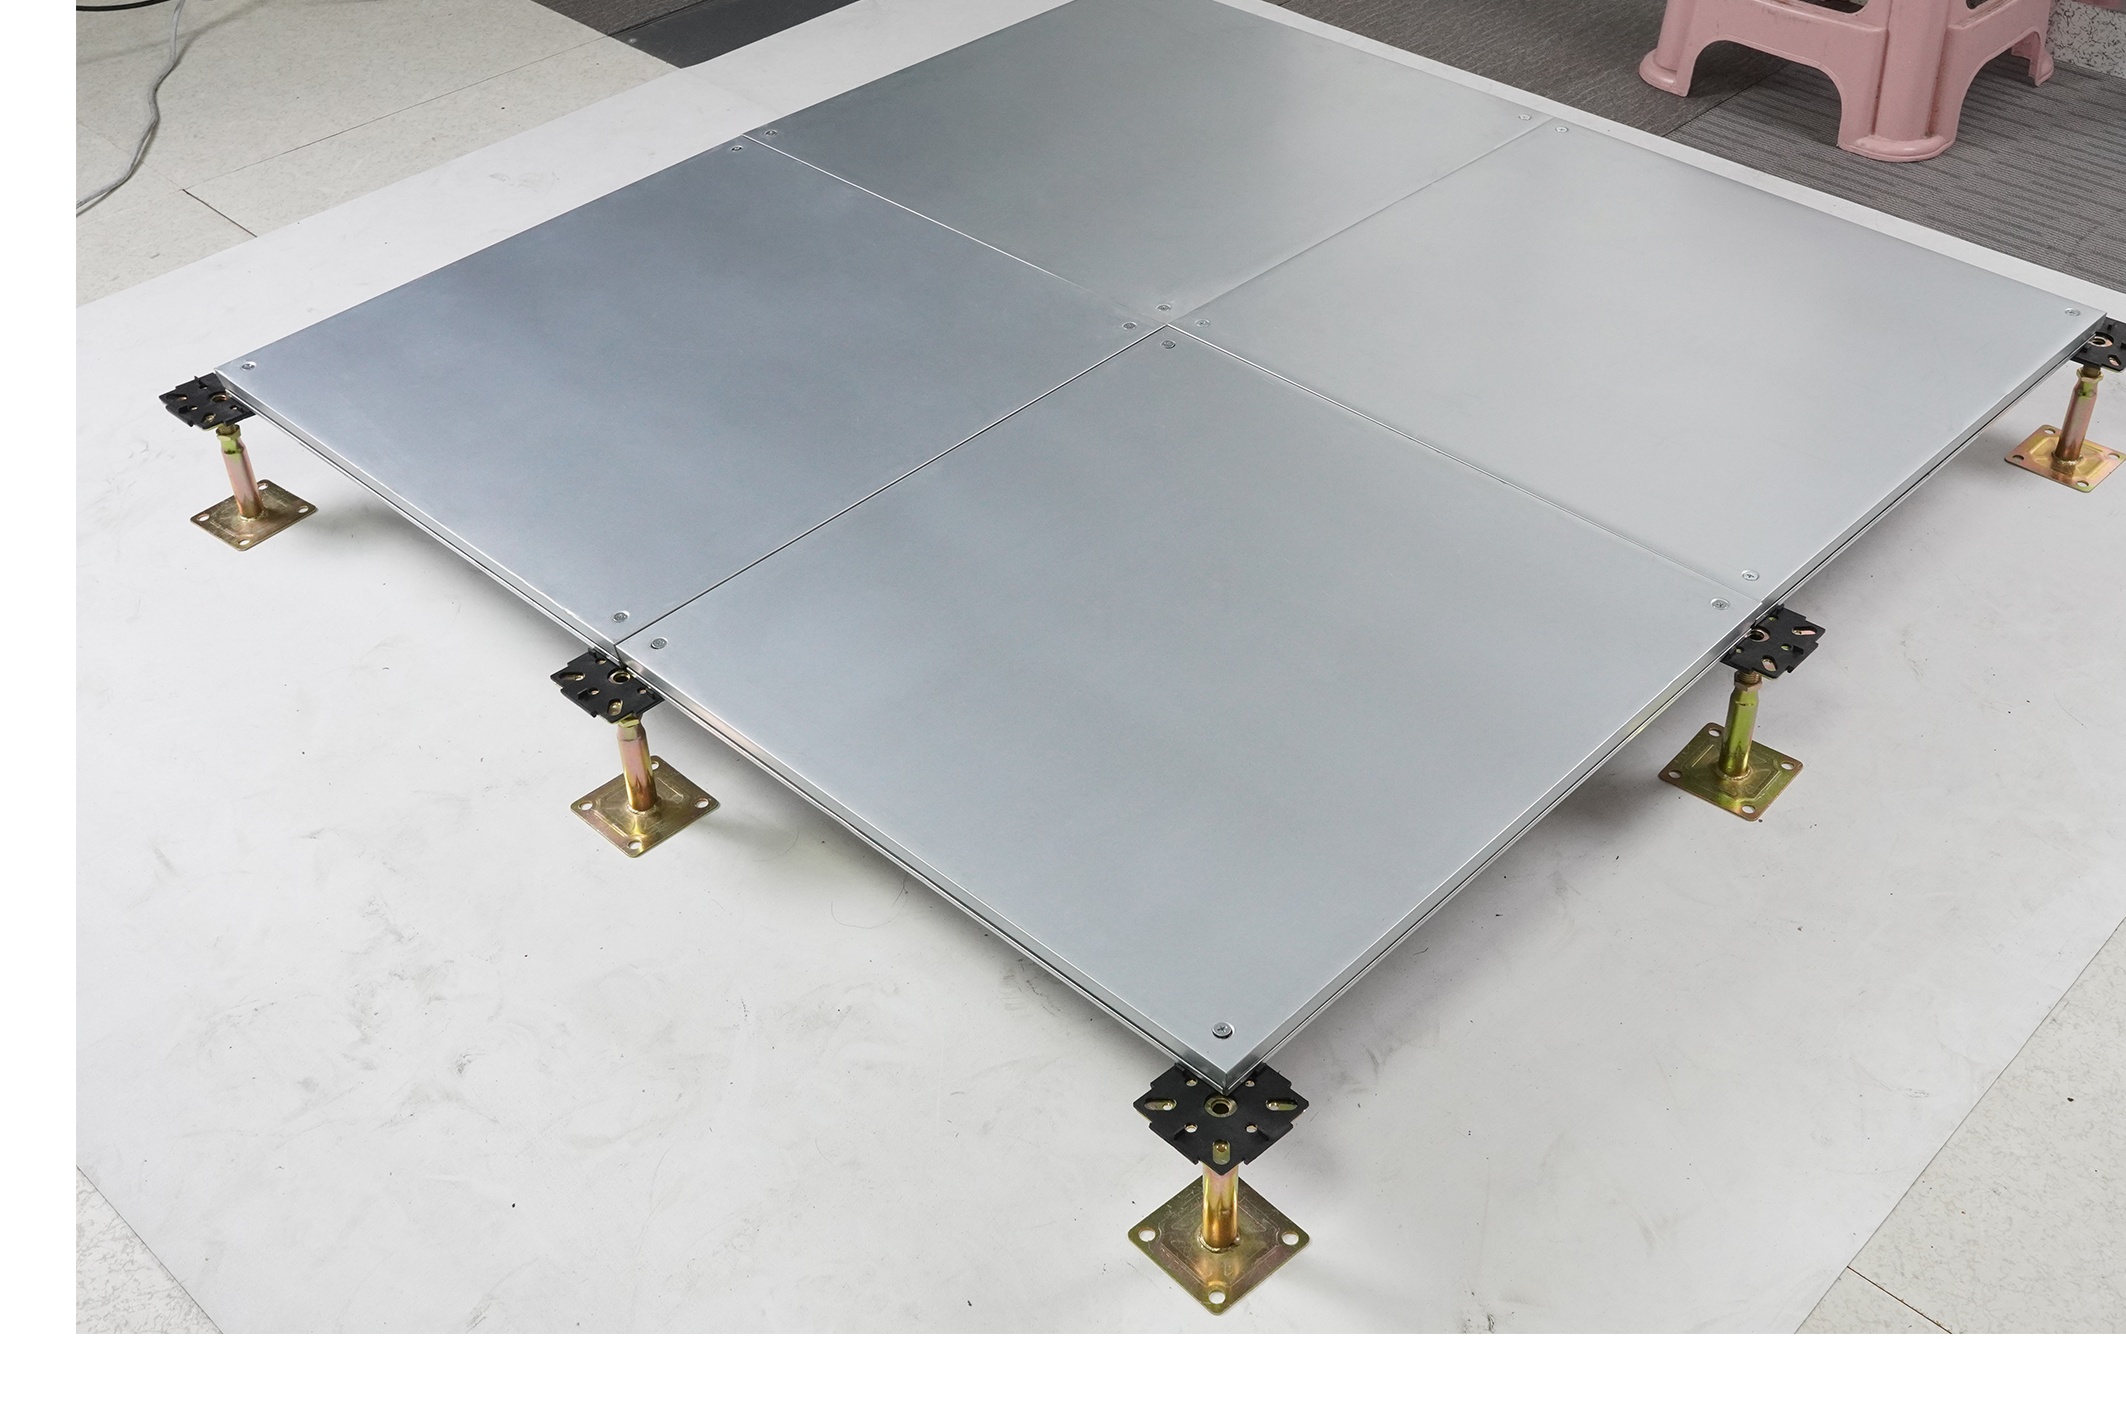
Choosing the right calcium sulfate six-sided steel-faced floor manufacturer can be the difference between a smooth installation and costly headaches. These access floors combine structural integrity with fire and sound resistance, but only if the manufacturer truly knows the craft. In this guide, we’ll break down the key factors—and introduce you to Lipin Floor, a brand worth knowing.
Where Six-Sided Steel Facing Earns Its Place in High-Traffic Floors
Hexagonal steel plates don't get installed by accident. In warehouses, loading docks, and factory corridors where forklifts rumble through every few minutes, flooring takes a beating that standard concrete or epoxy simply can't shrug off. The six-sided shape spreads impact loads more evenly than square or rectangular tiles, reducing the stress that leads to cracking around edges. That geometric advantage alone pushes many facility managers toward this solution when downtime for repairs isn't an option.
Another reason these plates hold their ground is the way they interlock under continuous traffic. Each side of a hexagon shares a boundary with a neighbor, creating a tighter, more stable surface that resists shifting and warping over time. You don't see the prying corners or lifting edges that plague other metal flooring systems in busy aisles. Maintenance crews appreciate that once the plates are set, they rarely need to reseat or replace individual pieces, even after years of heavy pallet jack use.
Safety also plays a starring role. The textured surface of six-sided steel facing offers reliable slip resistance, even when oils, greases, or rain get tracked inside. Workers move with confidence, and the plates' low profile means no tripping hazards from raised edges. For operations that can't afford a single shift of lost productivity, this kind of flooring quietly earns its keep without demanding constant attention.
How to Read a Calcium Sulfate Core Without Falling for Overload Specs
A lot of calcium sulfate core data sheets lead with one big number—usually an ultimate load or a dramatic overload claim. That figure gets recycled everywhere, but it rarely reflects how the panel behaves under everyday conditions. Instead of chasing the highest rating, check the test span, the support spacing, and whether the number comes from a point load or a uniform load.
Look for the distinction between failure load and allowable load. Manufacturers sometimes publish the first because it sounds stronger, but design values always sit below that threshold. If a sheet only gives you a single "overload spec" without a clear test standard, treat it as marketing rather than engineering. Ask for the moisture-conditioned flexural strength or the creep data, not just the breaking point.
Pay attention to how the core reacts after installation. Calcium sulfate can lose stiffness when exposed to high humidity or repeated wetting, so a dry-lab overload number may overstate real-world performance. A better reading includes long-term deflection, screw-holding capacity at expected moisture levels, and any edge-sealing requirements.
Locking Tolerances, Panel Flatness, and the Problems They Prevent
When panel assemblies rely on locking mechanisms, the allowable dimensional variation in the locking features directly determines how evenly the joined surfaces sit. A few tenths of a millimeter too much clearance at a tab or hook can let a panel shift under load, creating visible steps at seams and increasing the chance of rattles over time.
Panel flatness is not just a cosmetic target. Slight bowing or twist across a large panel can amplify small locking tolerances into misaligned edges and uneven gaps. Even when individual locks measure within spec, accumulated curvature across multiple fastening points can force the panel into a stressed state, leading to premature wear or microfractures around the mounting bosses.
Tightening locking tolerances and controlling flatness prevents three recurring failures: seam separation, localized stress whitening in plastic parts, and inconsistent latch engagement. The result is an assembly that feels solid on the first fit and stays quiet after repeated thermal cycles or vibration exposure.
Installation Day Details That Decide Whether a Floor Stays Quiet
Before the first plank is set, the subfloor has to be worked until it's flat within 3/16 inch over a 10-foot span. High spots get sanded down, low spots filled with a patching compound. If this step is rushed, the locking mechanisms carry extra stress and tiny gaps open up at the joints, which is where most squeaks and crackling sounds start. Loose subfloor panels need to be re-secured with screws, not nails, because nail pops later become a steady source of clicking underfoot.
Underlayment choice on installation day changes more than comfort. Even if the flooring comes with an attached pad, a separate roll of acoustic underlayment can cut down mid-range footfall noise. For glue-down work, trowel notch size matters. Too much adhesive leaves ridges that telegraph through the planks and create hollow, drum-like spots. Let the adhesive flash off properly before the flooring goes in; otherwise trapped solvent causes bubbles that crackle every time weight shifts over them.
The edge gaps are where many quiet floors fail. Leave a consistent 1/4 to 3/8 inch around the perimeter and at door thresholds. If planks are jammed tight against a wall, seasonal humidity will make them buckle or separate at the end joints, and that separation turns into a click with each step. Transition strips should not pinch the floor; a T-molding with enough vertical clearance lets the floor move without binding. Before baseboards and trim go on, walk every row slowly and listen for creaks, then fix loose areas while the adhesive is still workable.
Surface Choices for Offices, Labs, and Cleanrooms—Beyond the Default
Choosing a surface for an office, laboratory, or cleanroom usually starts with a short list of standard options—laminate, stainless steel, epoxy, maybe phenolic resin. But the conversation often stops there, as if those defaults automatically fit the actual work being done. What gets overlooked is how much the wrong surface quietly undermines daily operations: a lab bench that stains after the first solvent spill, a cleanroom table that sheds particles, or an office desk that looks tired within months. The real question isn't just which material is common, but which one survives the specific combination of chemicals, abrasion, temperature swings, and cleaning protocols in your environment.
Lab and cleanroom settings demand even deeper scrutiny. A surface that works fine for a microbiology lab may fail in a chemistry lab where acetone and strong acids are routine. Similarly, cleanroom classifications dictate not just smoothness but also outgassing, static dissipation, and compatibility with disinfectants like hydrogen peroxide or quaternary ammonium. Instead of accepting a default epoxy or stainless steel because it appears on every equipment list, focus on measurable criteria: chemical resistance over exposure time, particle retention after wiping, impact tolerance, and long-term cost per square foot including maintenance. For example, a modified solid surface might outperform stainless steel in a cleanroom because it can be seamlessly repaired on-site, reducing downtime and potential contamination risks.
Office environments have their own overlooked pitfalls. A high-gloss laminate may look sleek in a showroom but collects fingerprints and scratches in a busy collaborative space. A natural wood veneer adds warmth but warps near sunny windows or HVAC vents. And in hybrid offices, surfaces now face frequent disinfectant wiping, which can dull traditional finishes fast. By treating surface choice as a performance decision rather than a visual afterthought—testing swatches with the actual cleaning agents, checking edge durability, and asking about acoustics or heat transfer—you end up with spaces that stay functional and presentable years longer, without paying a premium for materials that were never a good fit in the first place.
What to Ask a Manufacturer When the Stakes Are Higher Than Price
When a production run carries real consequences—regulatory compliance, patient safety, brand reputation—the conversation has to move well beyond unit cost. You need to understand how the manufacturer handles failure. Ask for a documented corrective action process, and then push further: walk me through the last time a batch deviated from spec, what triggered it, and how you closed the loop with the customer. The quality of that story tells you more than any certificate on the wall.
Ask who actually touches your product at each stage. A small, dedicated team with direct accountability often beats a sprawling facility with impressive automation. Request the résumés of the process engineers and the quality manager, not just the sales contact. Find out how long the operator running your line has been in that role, and whether they are empowered to stop production if something looks wrong. In high-stakes manufacturing, hesitation to stop is the most expensive defect of all.
Finally, challenge them on supply chain transparency. Where do their raw materials come from, and how do they verify that origin under pressure? If a critical component suddenly becomes scarce, will you learn about the substitution before or after it ships? A trustworthy partner will have a clear, uncomfortable answer for that scenario—one that includes your team in the decision, not just a notification after the fact.
FAQ
The core is made from high-density calcium sulfate, which gives the panel excellent fire resistance, acoustic damping, and dimensional stability. Unlike chipboard or all-steel panels, it won't warp or rattle under heavy rolling loads. That combination makes it a favorite for offices, data centers, and equipment rooms where long-term flatness matters.
Encasing the calcium sulfate core on all six sides protects it from moisture, impact, and edge chipping during handling and installation. It also creates a continuous conductive path when the panels are grounded, which helps manage static electricity in sensitive electronic environments.
It means the top surface, bottom surface, and all four edges are covered with a steel layer, leaving no exposed core material. This full encapsulation strengthens the panel, improves its fire rating, and prevents the core from absorbing humidity that could cause swelling over time.
You'll often find it in data centers, control rooms, laboratories, and high-end office spaces with underfloor air distribution. The product's combination of high load capacity, fire safety, and acoustic isolation suits spaces where cabling and HVAC systems need to be easily accessible yet hidden.
Look beyond the spec sheet: ask about the steel gauge, the bonding method between steel and core, flatness tolerances, and third-party test reports for load and fire performance. A reliable factory should be able to show consistent batch testing and provide samples for independent verification.
Yes, most manufacturers offer options like HPL, vinyl, or carpet tile top finishes, as well as reinforced cores for heavier point loads or rolling loads. Custom sizes and cutouts for air grilles or cable outlets are also common, though they may affect lead time.
Routine cleaning is usually limited to vacuuming or damp mopping depending on the surface finish. If a panel becomes damaged, it can be lifted with a suction cup and replaced individually without disturbing the surrounding floor. Avoid using harsh solvents on the steel edges to preserve the protective coating.
The panels are designed to drop onto a pedestal head with stringer support, so trained crews can install large areas quickly. The main challenges are ensuring the subfloor is level and grounding the system properly. Once the grid is set, panel replacement and reconfiguration are straightforward.
Conclusion
Calcium sulfate access floors with six-sided steel facing earn their place in high-traffic environments because every face of the panel is protected, not just the top. This full encapsulation stops moisture ingress, edge chipping, and core crumbling that commonly shorten the lifespan of standard raised floors. But don't let overload specs mislead you—what really matters is how the calcium sulfate core performs under sustained loads and point loads. A quality manufacturer will tell you the panel's density, curing time, and how the steel shell is bonded, rather than simply quoting a higher ultimate load. Tight locking tolerances and panel flatness are non-negotiable if you want to avoid squeaks, rocking panels, and visible lippage that turn a premium floor into a maintenance headache.
Installation day often decides whether the floor stays quiet for a decade or starts complaining after two years. Proper substrate leveling, adhesive coverage, torque on pedestal bolts, and edge alignment all play a bigger role than most spec sheets admit. Surface choices should move beyond the default HPL: for offices you might want acoustic backing, for labs a chemical-resistant finish, for cleanrooms a static-dissipative coating that won't shed particles. When the stakes are higher than price, ask the manufacturer for independent test reports under realistic load scenarios, actual flatness tolerance measurements, warranty terms that cover edge and underside protection, and lead times for matching replacement panels. A supplier that answers these directly is the one you can trust for long-term floor performance.
Contact Us
Contact Person: yuki
Email: [email protected]
Tel/WhatsApp: +86 18664390732
Website: https://www.lipinfloor.com/